Low-MOQ OEM/ODM manufacturing solutions built to rigorous European & International technical benchmarks.
Eliminating offshore supply chain friction through UK-directed governance and direct facility ownership.
Combining London-based account direction, native English tech-pack communication, and UK contract security with the cost efficiency of an owned overseas manufacturing facility.
Scale your brand without tying up working capital. Test capsule drops, analyze market acceptance, and iterate sizing patterns before committing to high-volume manufacturing runs.
Every batch undergoes incoming raw material testing, in-line seam integrity auditing, end-of-line dimensional grading verification, and pre-pack AQL inspections.
The global textile apparel manufacturing ecosystem is undergoing a structural transformation driven by stringent regulatory frameworks, eco-conscious consumer behavior, and the rapid adoption of digital prototyping workflows. For modern apparel brands, emerging designers, and retail enterprises, selecting a CE Certified Apparel Development Manufacturer and Exporter is no longer simply about minimizing FOB costs—it is a critical strategic decision that dictates supply chain resilience, brand equity, and compliance safety.
Key Insight for Sourcing Directors: CE certification in garment development guarantees that raw materials, dyes, functional hardware, and structural seams conform to strict European health, safety, and environmental protection standards (including REACH SVHC compliance and EN ISO standards for mechanical safety).
Navigating cross-border apparel distribution requires strict adherence to international safety standards. CE certification signifies that garments adhere to essential health and safety mandates outlined in European directives. In modern activewear, protective loungewear, and heavy fleece streetwear, compliance extends across multiple chemical and structural parameters:
Traditional apparel sourcing models enforced minimum order quantities (MOQs) of 500 to 1,000 units per colorway. This obsolete procurement strategy routinely leads to overproduction, deadstock inventory, and severe cash flow bottlenecks. The future of global apparel sourcing is anchored on three foundational pillars:
Deploying initial production runs from 50 to 100 units. Brands evaluate real-world consumer conversion rates before triggering scalable automated bulk reorders.
Utilizing 3D CAD stress-testing (CLO3D / Browzwear) to render fabric drape, stress points, and pattern grading digitally, reducing physical sampling cycles by 70%.
Transitioning to GOTS-certified organic cotton, Recycled Polyester (rPET), and low-impact eco-dye acid washing to satisfy corporate ESG directives.
Achieving superior product positioning in the streetwear, sportswear, and private-label sectors requires absolute control over fabric composition, grammage (GSM), and finishing treatments. As a dedicated OEM/ODM exporter, our facility engineers fabrics from yarn level to finished piece:
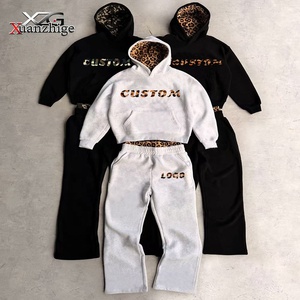
Heavyweight Fleece Engineering (400 GSM – 500 GSM): Used extensively in our custom hoodie and jogger lines, our 100% combed cotton and 60/40 CVC fleece fabrics utilize a 3-thread double-faced loopback construction. This creates an impenetrable barrier against cold climates while preventing fleece shedding and interior fiber linting during wear.
Functional Synthetic & Windbreaker Engineering: Our 3M reflective nylon windbreaker sets combine lightweight 100% high-density polyamide shells with breathable micro-mesh interiors. Water-repellent DWR coatings are applied alongside glass-bead reflective heat transfer tech to deliver EN ISO 20471 compliance for night-time visibility and thermal protection.
Vintage Acid Wash & Garment Dyeing Mechanics: Achieving high-end vintage aesthetics without destroying fiber tensile strength requires specialized ozone wash and eco-enzyme stone wash processing. Our wet-processing lab continuously monitors pH balances and tensile loss metrics to preserve seam durability while delivering soft-hand distress effects.
Our end-to-end manufacturing workflow guarantees complete transparency, zero-defect pattern scaling, and predictable delivery windows from initial design consultation to global fulfillment.
Digitizing your visual sketches into production-ready specifications, defining bill of materials (BOM), stitch per inch (SPI) counts, and graded measurement charts.
Precision pattern cutting using automated CAD systems. Graded across S to XXL sizing spectrums to eliminate fit distortion across different body types.
Yarn sourcing, circular knitting, and custom Pantone color matching (Lab dip approval with Delta E < 0.8 color variance tolerance).
Production of a physical golden sample. Every detail—from embroidered logos to custom neck labels—is reviewed and signed off prior to bulk execution.
Operated by skilled garment technicians using multi-needle cover-stitching, flatlock seam reinforcement, and synchronized line assembly.
Comprehensive AQL 2.5 major / 4.0 minor inspections, metal needle-detection scanning, steam pressing, custom polybag packaging, and door-to-door delivery.
Direct technical answers regarding compliance, production lead times, fabric specs, and ordering procedures.
Our CE certified development protocol ensures full alignment with European Personal Protective Equipment (PPE) standards where applicable, as well as general textile safety directives. This includes REACH regulation (EC) No 1907/2006 compliance for non-toxic chemical dyes, EN ISO 14116 for limited flame spread (if required for technical wear), and EN ISO 13688 general ergonomics. Every raw material roll is tested for heavy metals, formaldehyde, and color fastness under friction and washing.
Unlike broker agencies, we directly own and manage our overseas manufacturing production lines. We maintain an extensive raw material inventory of pre-tested, high-grade knit fabrics (such as 300-450 GSM fleece, 180-240 GSM single jersey cotton, and nylon windbreaker shells). By utilizing digital CAD pattern layout software and specialized micro-line sewing setups, we can cut and sew custom 50-piece batches efficiently without incurring high setup overheads.
While a fully detailed tech pack (including flat sketches, seam callouts, stitch types, BOM, and measurement spec sheets) speeds up initial quotation, it is not mandatory. If you only possess fashion sketches, physical reference samples, or preliminary mood boards, our in-house garment design engineers will construct a complete, repeatable technical tech pack for your approval prior to prototype cutting.
Sample development and prototype delivery generally require 2 to 3 weeks, depending on whether custom fabric knitting or specialized acid wash finishing is required. Once the physical golden sample is approved, bulk manufacturing takes 4 to 6 weeks. We provide a milestone-tracked production schedule prior to deposit payment, ensuring complete timing visibility for seasonal retail drops.
We utilize the Pantone Matching System (PMS Textile Cotton / Polyester System). During raw fabric preparation, our laboratory creates 3-option lab dips (spectrophotometer tested) for client sign-off under D65 daylight, TL84 store lighting, and UV light conditions. We keep strict digital master swatches on file to guarantee zero shade variation across repeat bulk drops.
Our production floor is equipped for high-density 3D puff screen printing, Direct-to-Garment (DTG), sublimation, chenille patching, flat/3D embroidery, reflective 3M transfers, custom branded YKK hardware, jacquard drawcords, and custom woven neck and care labels. We also offer fully customized eco-friendly polybags and retail presentation boxes.
Contact our UK merchandising team today to discuss your tech pack specifications, request fabric swatches, or initiate your 50-piece custom sample order.
Send an Inquiry