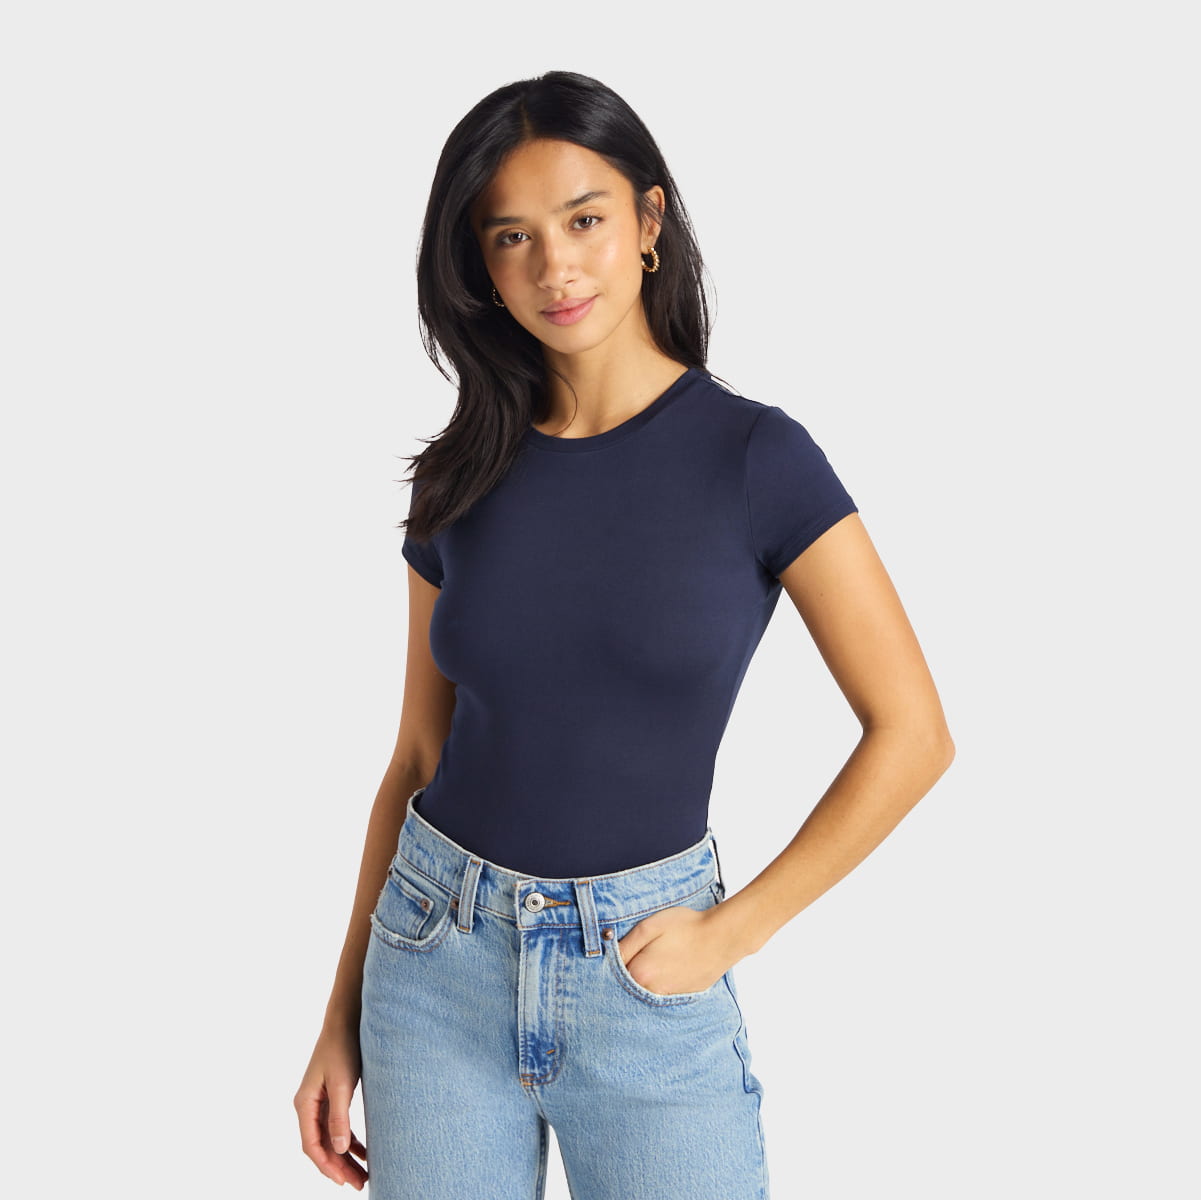
Technical custom gym wear manufacturing facility producing high-performance activewear
Handcrafted precision sewing for custom gym wear and compression apparel
High performance activewear and custom gym apparel ready for global distribution
Technical Activewear Sourcing · Low MOQ From 50pcs

Custom Gym Wear Manufacturing: Technical Sourcing & Low-MOQ Scaling Guide

Engineering premium activewear for global brands. From squat-proof fabrics and 4-needle flatlock stitching to 3D pre-production trialling and 4-stage quality control under UK contract terms.

50 PcsLow MOQ Per Custom Design
2,000+Global Brands Supported
4-StageIn-House Quality Control
100%Squat-Proof & Fit Verified
Enterprise Activewear Sourcing

Navigating Technical Custom Gym Wear Manufacturing with Direct Factory Control

In the hyper-competitive global activewear landscape, sourcing high-performance fitness garments requires far more than basic print-on-demand or white-label re-branding. Technical buyers, procurement heads, and visionary activewear founders face complex structural challenges: eliminating fabric sheer under maximum elongation (the squat-proof requirement), securing 4-way stretch elasticity without elastane degradation, preventing seam chafe, and managing capital efficiency during initial drops.

Hawthorn International bridges the gap between low-volume agile releases and uncompromising factory-direct manufacturing. Headquartered in Central London with our own fully owned overseas production facility, we offer complete UK legal governance, English-speaking technical merchandising, and full transparency. Every custom gym wear order — starting from just 50 pieces per design — undergoes full pattern development, 3D pre-production digital trialling, Pantone-matched fabric sourcing, and rigorous 4-stage quality control.

Inquire Now Our Factory Advantage
Technical Engineering

The Anatomy of High-Performance Custom Gym Wear

True athletic performance is unlocked at the microscopic fiber level. We engineer activewear designed to endure intense kinetic stress, moisture accumulation, and high friction.

1. Advanced Fiber Matrix

We source and custom-knit high-density blends of recycled Nylon 6,6, Micro-Polyester, and genuine Lycra® (elastane content up to 25%). This creates an ultra-soft second-skin handfeel with non-sheer opacity under 100% stretch extension.

  • Nylon 6,6 for extreme tensile strength
  • Hydrophilic moisture-wicking coatings
  • PFAS-free durable water repellent (DWR)

2. Precision Seam Engineering

Standard overlock stitching causes friction and skin abrasion during workouts. We deploy 4-needle 6-thread flatlock machines and ultrasonic seam bonding for flush, lay-flat seams that expand continuously with movement.

  • ISO 607 Flatlock seam execution
  • Reinforced stress points & bar-tacking
  • Seamless circular knitting options

3. Ergonomic Pattern & Grading

Our pattern masters cut patterns specifically engineered for athletic posture. Sizing models are digitally graded in 3D across full size ranges (XS to 4XL) to ensure compression ratios remain identical regardless of body type.

  • Custom rise heights & stay-put waistbands
  • Gusseted crotch constructions
  • Anatomic body-mapping panels

Target Specifications by Performance Category

Selecting the right Grams per Square Meter (GSM) and fiber composition is critical for thermal regulation, durability, and squating security.

Category Optimal GSM Recommended Composition Key Features & Finishes
High-Impact Compression Leggings 260 – 320 GSM 75% Nylon 6,6 / 25% Lycra® Interlock double-knit, 4-way stretch, 100% squat-proof opacity, high waistband.
Maximum Support Sports Bras 280 – 340 GSM 78% Recycled Polyester / 22% Spandex Moisture-wicking mesh lining, removable molded cups, reinforced under-bust band.
Lightweight Performance Tees 140 – 180 GSM 92% Polyester / 8% Elastane Micromesh ventilation, silver-ion antibacterial treatment, quick-dry finish.
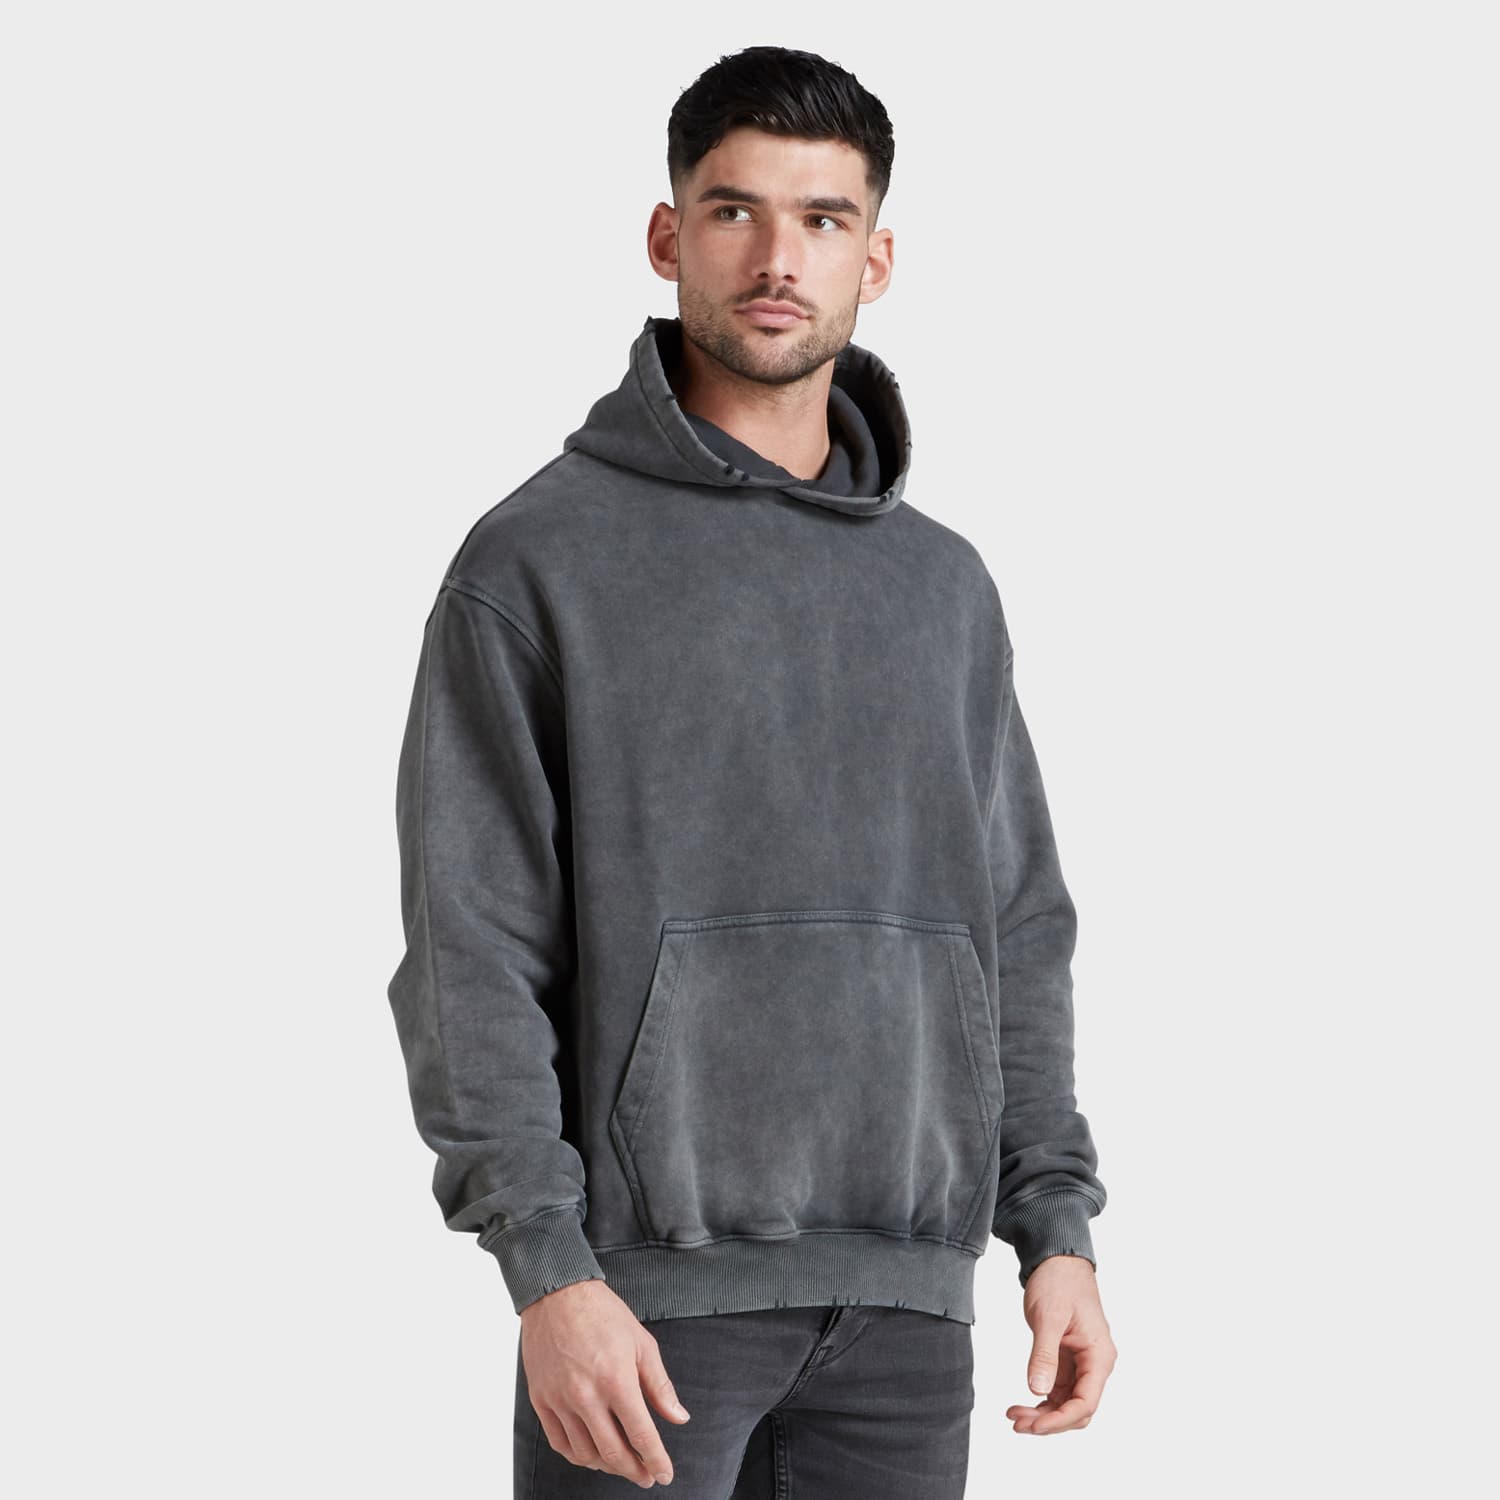
Heavyweight Pump Covers 280 – 400 GSM 100% Heavyweight Combed Cotton Drop-shoulder streetwear cut, silicone enzyme wash, shrink-free pre-shrunk fleece.
Technical Training Shorts 160 – 210 GSM 88% Nylon / 12% Spandex Outer 4-way stretch woven, hydrophobic DWR finish, lightweight compression liner.
The Hawthorn Model

Why Fast-Growing Activewear Brands Partner with Us

Traditional overseas apparel factories force high MOQs and operate behind opaque broker networks. Hawthorn combines direct factory execution with the trust, security, and communication of a London-based company.

01 / Low MOQ Flexibility

50 Pieces Per Design — Preserve Capital, Test Markets

Launch limited-edition capsules or evaluate new activewear fits without over-committing cash flow. We support low minimum order quantities from 50 pieces per style across custom colorways and size splits.

02 / Factory Ownership

Direct Factory Ownership

We own our overseas manufacturing facility. No middleman markups, full production schedule control, and direct line visibility.

03 / Tech Development

3D Pre-Production Trialling

Visualize, stress-test fit, and refine garment construction digitally in 3D prior to cutting physical fabric, minimizing revision cycles.

Precision quality inspection during custom gym wear manufacturing
04 / Quality Control

4-Stage QC Protocol

Fabric shade/fault check, in-line seam integrity audit, dimensional size chart check, and final pre-pack inspection.

05 / Legal Governance

UK Legal Contracts & London Headquarters

Hawthorn International Ltd (Company No. 08937806) operates under strict UK contract law. Brief your dedicated London account team in native English while accessing true factory-direct manufacturing costs.

Product Capabilities

Custom Gym Wear Manufacturing Product Ranges

From performance compression activewear to athleisure pump covers, we build custom garments engineered around your exact brand specifications.

Custom high-impact sports bras and compression activewear sets
Seamless & Cut-and-Sew Leggings

Squat-Proof Performance Compression Leggings

Designed for powerlifting, cross-training, and high-intensity workouts. Our leggings feature dual-layer high waistbands that lock into position without rolling down, hidden waistband pockets for storage, and strategic contour shading.

Utilizing high-gauge interlock knitting with 25% elastane, we guarantee zero sheer transparency under maximum stretch conditions during lab squat testing.

  • High waistband with core compression lining
  • Optional gusseted or seamless crotch construction
  • High-density reflective silicon logo printing
Custom gym tees and breathable training apparel
T-Shirts & Oversized Covers

Technical Training Tops & Streetwear Pump Covers

Whether your line targets heavy bodybuilding aesthetic or sleek minimalist activewear, we produce the exact fit profile required. Choose from moisture-wicking micro-polyester tees with laser-cut ventilation holes or heavyweight 320 GSM vintage-washed cotton pump covers.

Custom tailoring details include anti-chafing back neck taping, extended curved hems for overhead lifting, and split side vents.

  • Custom fabric weights from 140 GSM micro-mesh to 400 GSM fleece
  • Antibacterial silver-ion and quick-dry finishes
  • DTG, Screen print, high-density 3D rubber, & puff print options
Custom gym hoodies and technical activewear jackets gallery
Outerwear & Layering

Technical Gym Hoodies, Tracksuits & Outerwear

Complete your brand line-up with engineered outer layers built for warm-ups, outdoor conditioning, and post-workout recovery. We develop custom technical hoodies, zip jackets, and tapered trackpants featuring waterproof zippers and ergonomic thumbhole cuffs.

Choose between warm brushed-back fleece or lightweight 4-way stretch woven softshell fabrics treated with durable water resistance.

  • Waterproof heat-sealed zipper garages
  • Custom dip-dyed drawcords and heavy matte hardware
  • Ergonomic raglan sleeve designs for full shoulder mobility
Industry Insights

Future Procurement Trends in Custom Gym Wear Manufacturing (2026–2030)

The global activewear sector is undergoing rapid transformation driven by technological innovation, environmental mandates, and changing consumer purchasing behaviors. Sourcing directors must anticipate these structural shifts to protect margin integrity and brand relevance.

Trend 01

Circular & Bio-Based Synthetics

Brands are shifting away from virgin polyester toward GRS-certified ocean-bound recycled nylon, bio-based spandex derived from renewable cornstarch, and mono-material recyclable garments that simplify end-of-life recycling.

Trend 02

AI 3D Prototyping & Virtual Sampling

Digital twin technology allows brand managers to sample fit, tension maps, and print placement in 3D prior to cutting fabric. This reduces physical sampling waste by 75% and accelerates speed-to-market by up to three weeks.

Trend 03

Agile Low-MOQ Supply Chains

The traditional model of ordering 5,000 units per colorway six months in advance creates inventory risk. Modern brands rely on micro-batch sourcing (50–300 units) to test demand on social platforms before triggering rapid re-orders.

Trend 04

Hybrid Functional Fitness Wear

The rise of hybrid training modalities (such as Hyrox, CrossFit, and triathlon conditioning) demands garments that seamlessly blend extreme breathability with tear-resistant abrasion resistance against barbells and turf.

Handcrafted custom activewear stitching and finishing
Industry Evolution

Innovations Transforming Fitness Apparel Manufacturing

Modern consumers demand activewear that performs flawlessly in the gym while transitioning naturally into everyday lifestyle settings. Achieving this balance requires constant innovation in finishing techniques, branding execution, and fabric treatments.

Hawthorn continually integrates cutting-edge textile technologies into our custom gym wear production line:

  • Smart Antibacterial Finishes: Non-toxic zinc and silver-ion treatments embedded into fibers to destroy odor-causing bacteria permanently.
  • High-Density Silicone Transfer branding: Stretchable, non-cracking 3D heat transfers that endure over 100 industrial wash cycles.
  • Seamless Body-Mapping: Circular knitting zones that integrate ventilation mesh directly into high-sweat areas without added seams.
  • PFAS-Free Waterproofing: Environmentally compliant hydrophobic coatings for outdoor conditioning gear.
Step-by-Step Workflow

Our End-to-End Gym Wear Production Route

We manage every technical phase of your custom gym wear order — taking your raw sketches or reference garments and transforming them into market-ready retail products.

STEP 01 Pre-production 3D activewear trial

Pre-Production & 3D Trial

We review your brief, target markets, and pricing targets. Designs are digitalized and trialled in 3D to refine seam lines and fit before cutting fabric.

Digital stress testing for stretch & fit accuracy.

STEP 02 Activewear pattern cutting and grading

Pattern Cutting & Grading

Master athletic patterns are cut by hand or CAD. Sizing is graded precisely across your full size matrix to guarantee consistent activewear fit.

Custom rise, inseam, and compression grading included.

STEP 03 Performance activewear fabric sourcing

Performance Fabric Sourcing

We source custom-knitted nylon, recycled polyester, or organic cotton. Custom Pantone dyeing ensures absolute brand color consistency across batches.

Lab-tested for GSM, opacity & stretch recovery.

STEP 04 Activewear sample creation and approval

Prototype Sampling

A physical pre-production sample is crafted and delivered for review. Wear-test your leggings or sports bra to confirm fit, feel, and performance.

One sample unit included with every bulk order.

STEP 05 Hand-stitched bulk activewear production line

Bulk Manufacturing

Upon sample approval, your order enters our owned factory line. Skilled seamstresses hand-stitch panels using flatlock machines to ensure seam strength.

Cut & sewn by hand to approved specifications.

STEP 06 4-Stage quality inspection and global shipping

4-Stage Quality Check & Dispatch

Every single unit passes 4 distinct QC checks for stitch integrity, measurement tolerance, and opacity before custom packaging and global dispatch.

Tracked air/sea logistics to your facility door.

Activewear Capabilities & Specialties

Seamless Compression Leggings High-Impact Sports Bras Moisture-Wicking Gym Tees Oversized Pump Covers 4-Way Stretch Training Shorts Thermal Active Hoodies Tapered Gym Trackpants Cropped Tops & Tanks Bodybuilding Stringers Seamless Cycling Shorts Custom Woven Waistbands High-Density Rubber Prints
Procurement FAQ

Frequently Asked Questions on Custom Gym Wear Manufacturing

Detailed technical and commercial answers to the questions global brand founders, sourcing managers, and procurement leads ask when sourcing activewear partners.

Inquire Now

Unit pricing in custom gym wear manufacturing is determined by four primary cost drivers: fabric yield (GSM and composition), seam complexity (e.g., 4-needle flatlock vs standard overlock), branding execution (silicone print, jacquard elastic, embroidered logos), and total production volume.

At a 50-piece minimum order quantity (MOQ), fixed setup costs (such as master pattern development, grading, digitizing print screens, and machine calibration) are amortized over fewer garments, resulting in a higher cost-per-unit. At 1,000 units, fabric mills provide volume discounts on raw yarns and Pantone dyeing, reducing per-unit manufacturing costs by 35% to 50%.

Hawthorn offers full cost transparency prior to production. We optimize your tech pack to maximize profit margins at both low 50-piece launch runs and high-volume repeat runs.

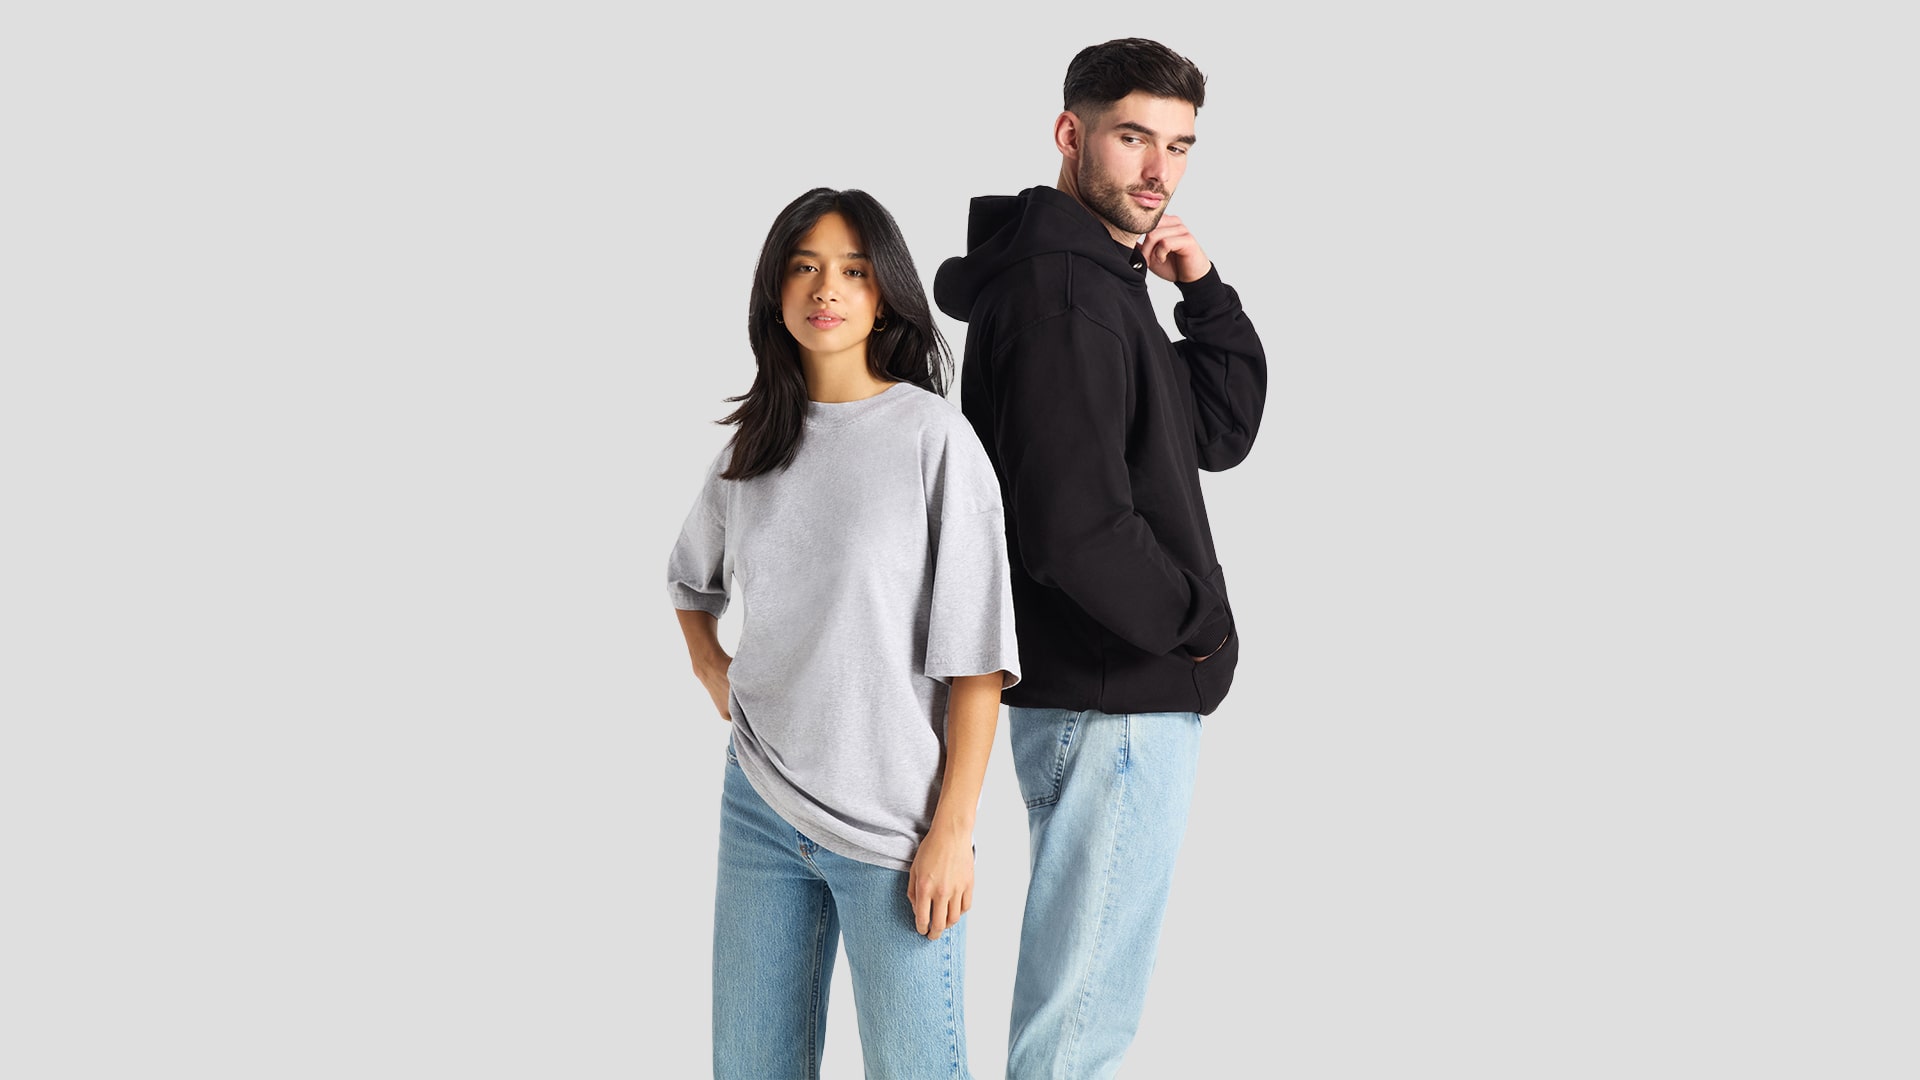
Fabric sheer (transparency failure during deep squats or stretches) occurs when low-gauge fabric is stretched beyond its knit density, causing light to pass between stretched yarns. Many cheap suppliers attempt to cut costs by using thin single-jersey knits under 220 GSM.

Hawthorn guarantees squat-proof opacity by engineering high-gauge Interlock Double-Knit structures with a minimum fabric weight of 260 to 300 GSM. Interlock knitting utilizes two sets of needles to create two overlapping fabric layers knitted face-to-face, ensuring that even under 100% horizontal tension, light penetration is eliminated. Every fabric batch undergoes physical stretch-board lab audits prior to cutting.

Activewear tech packs require significantly higher technical detail due to garment elasticity and dynamic functional movement. Critical data points include:

1. Fabric Stretch Percentage & Recovery Index: Specific vertical and horizontal modulus requirements (e.g., 80% stretch / 98% recovery rating).
2. Stitching Specifications: ISO stitch types (e.g., ISO 607 4-needle flatlock) and SPI (Stitches Per Inch, typically 10–12 SPI for activewear seams).
3. Ergonomic Point of Measurements (POM): Extended measurements for relaxed vs fully stretched waistband, thigh circumference, gusset drop, and armhole elasticity.
4. Trims & Hardware: Sweat-resistant coated eyelets, rubber-tipped drawcords, and heat-transfer placement coordinates.

If you do not have a completed tech pack, Hawthorn’s technical apparel team will construct one for you from your physical reference samples or design concepts.

Standard fabric dyeing mills typically mandate minimum dye-lot quantities of 300 kg to 500 kg per color. For small-batch activewear drops, this can present a significant inventory hurdle.

Hawthorn maintains strategic relationships with specialized lab-dye facilities that accept low-volume sample dyeing. We utilize Pantone Fashion, Home + Interiors (TCX/TPX) color codes. Before bulk fabric dyeing commences, we produce lab dips (small dyed fabric swatches) for your visual inspection and approval under standardized D65 lighting environments, ensuring exact brand palette consistency across different product styles.

Production timelines are divided into three distinct operational phases:

1. Development & Sampling (2 to 4 Weeks): Includes pattern creation, 3D pre-production trialling, fabric lab dips, and physical prototype construction.
2. Sample Approval & Revisions (1 Week): Your team wear-tests the physical sample and approves or requests minor fit adjustments.
3. Bulk Manufacturing (4 to 6 Weeks): Fabric knitting, dyeing, precision cutting, flatlock stitching, 4-stage quality control, and custom packaging.

Your dedicated UK account manager provides a milestone timeline chart before production starts, allowing you to plan launch marketing with complete confidence.

As a UK registered business (Hawthorn International Ltd), we are legally bound to enforce ethical, transparent, and fair working standards throughout our entire supply chain. Because we operate our own manufacturing facility overseas rather than placing orders through unverified sub-contractors, we directly enforce:

• Fair living wages, regulated 8-hour work shifts, and paid overtime.
• Safe, climate-controlled working conditions with modern ergonomics.
• Zero tolerance for child labor, forced labor, or unsafe factory practices.
• Sourcing of Global Recycled Standard (GRS) certified yarns and OEKO-TEX® Standard 100 non-toxic fabric dyes.

Fabric pilling and loss of stretch elasticity occur when short-staple fibers break under surface friction or when cheap spandex degrades under friction and sweat exposure.

We eliminate these failure points by utilizing long-filament continuous synthetics (high-multi Nylon 6,6) and heat-set elastane yarn matrixes. Additionally, our fabrics undergo anti-pilling singeing and silicone wash treatments that pass Martindale Abrasion Tests exceeding 20,000 cycles, guaranteeing long-lasting shape retention wash after wash.

Get Started Today

Ready to Launch or Scale Your Custom Gym Wear Collection?

Partner with a UK-managed, direct-factory activewear manufacturer. Share your tech packs, reference photos, or design concepts and our merchandising team will generate a comprehensive quote, fabric recommendations, and lead time schedule.

Inquire Now