
Low MOQ Production Starting at 50 Pieces
Test new silhouettes, introduce seasonal color drops, and validate audience demand without over-committing cash flow. Expand to thousands of units seamlessly as your sales velocity accelerates.
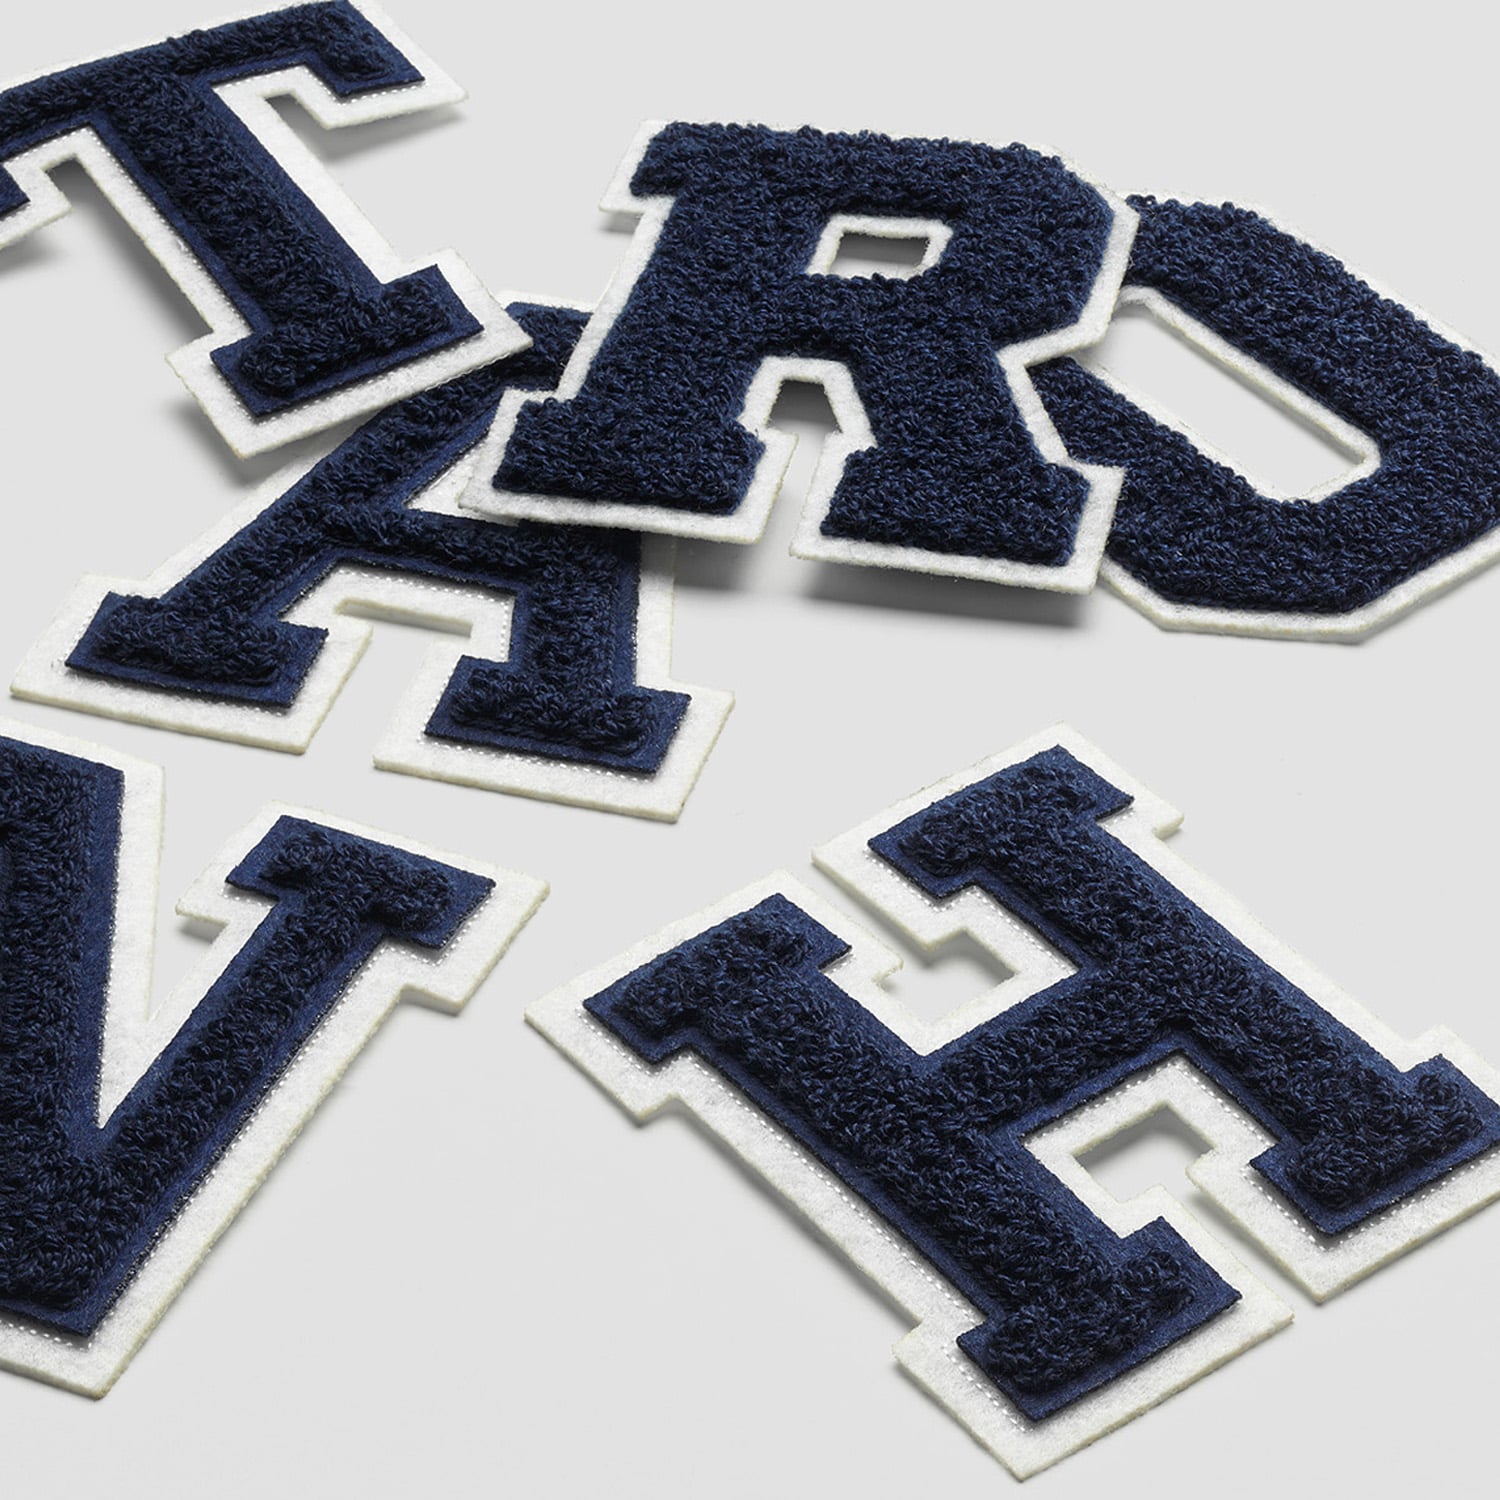
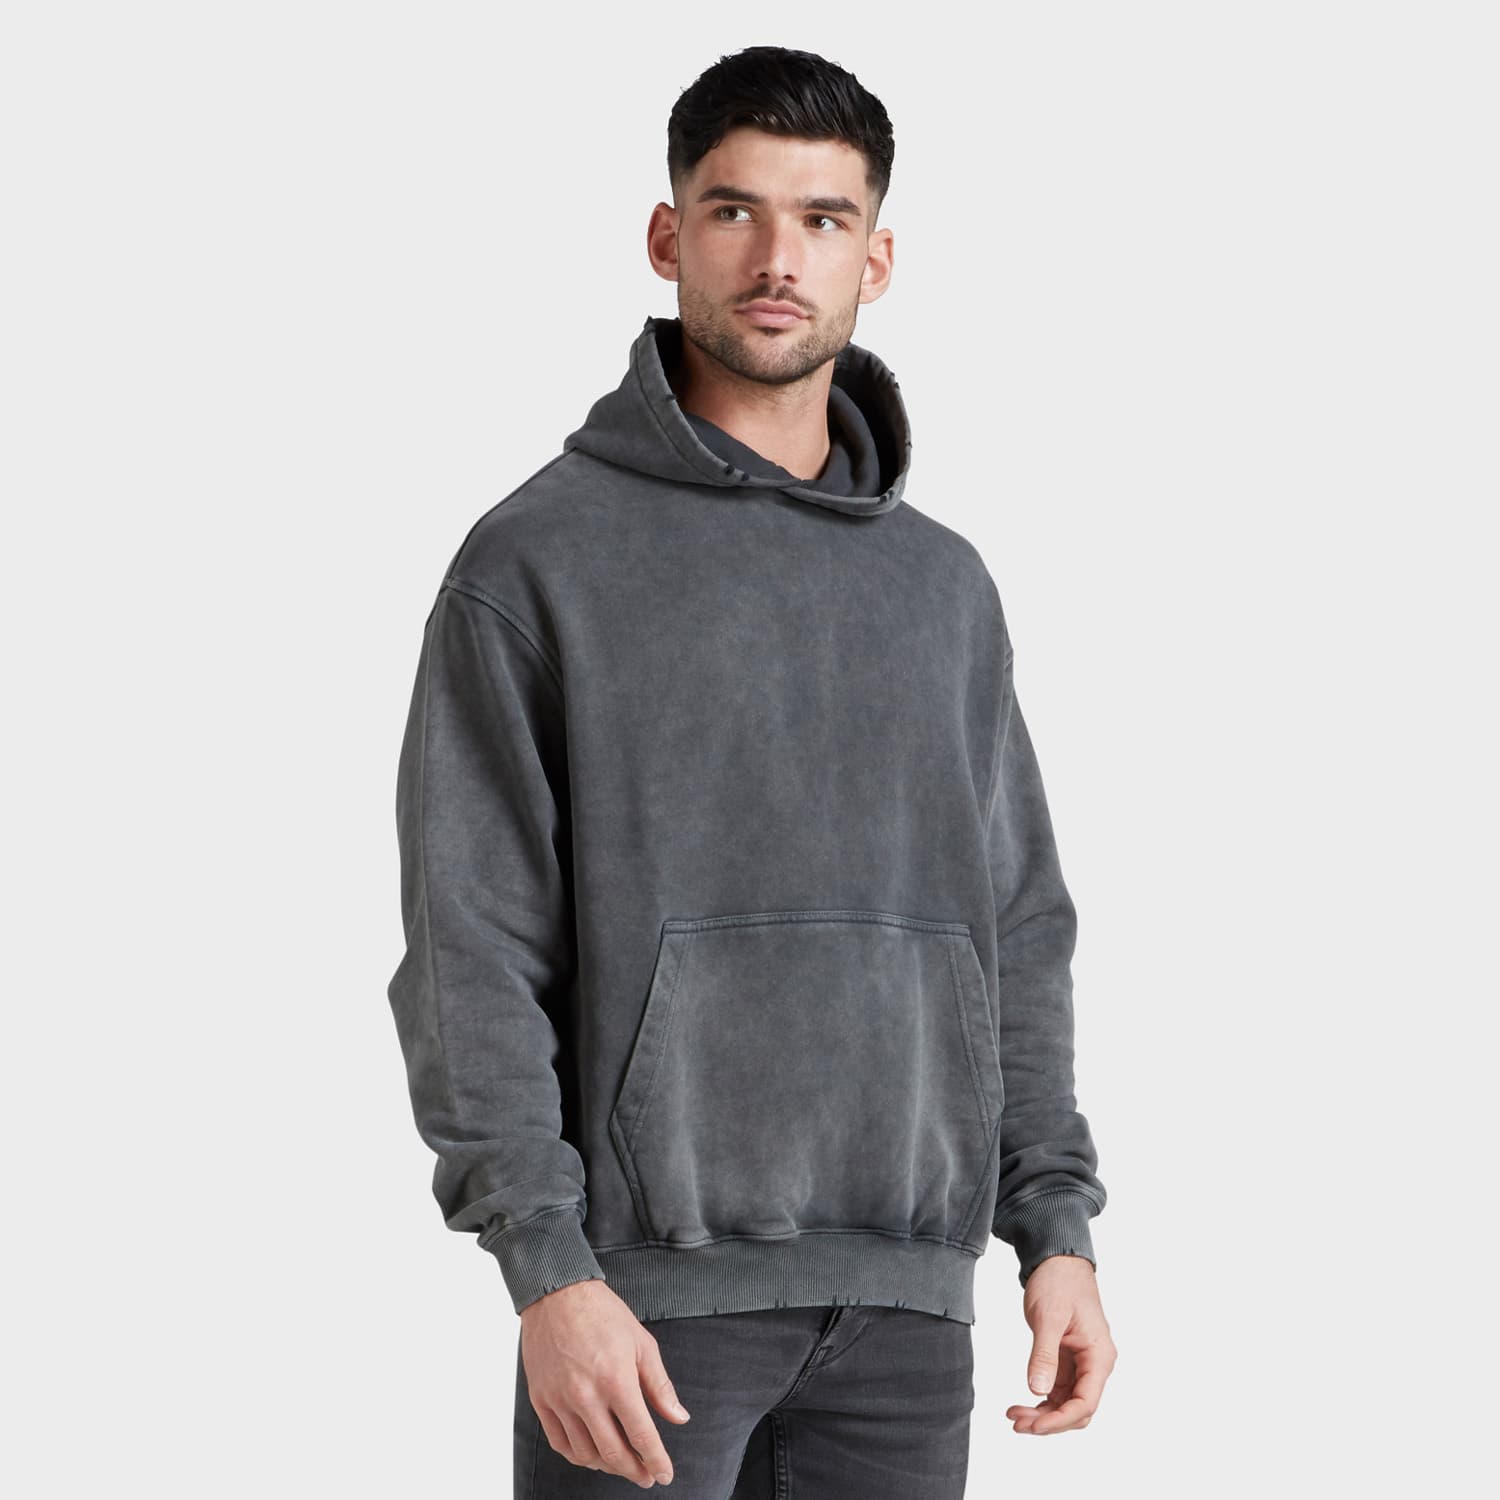
From custom organic cotton French terry to bamboo modal lounge sets. Low minimums, direct factory control, and full UK account management.
The global loungewear market has evolved permanently. No longer restricted to basic sleepwear or oversized home leisure garments, modern loungewear occupies a high-margin intersection between luxury casualwear, streetwear silhouettes, and high-performance tactile comfort. For fashion entrepreneurs, direct-to-consumer (D2C) apparel brands, and boutique retail directors, sourcing a reliable private label loungewear manufacturing partner is the single most critical structural decision in building a profitable collection.
At Hawthorn International, we bridge the historical divide between low-volume startup agility and commercial scale. Headquartered in Central London with our own fully owned overseas production facility, we eliminate broker markups, enforce strict European contract guarantees, and offer true cut-and-sew customization starting at just 50 pieces per design.
Traditional apparel factories force brands into 500+ unit minimums per colorway, leading to tied-up working capital and stock liability. Off-the-shelf blank suppliers offer low MOQs but compromise fit uniqueness, fabric handfeel, and brand identity. Hawthorn offers a hybrid model built for sustainable growth.
Test new silhouettes, introduce seasonal color drops, and validate audience demand without over-committing cash flow. Expand to thousands of units seamlessly as your sales velocity accelerates.
We do not print on stock blanks. Every garment is cut, stitched, and finished to your precise size chart and pattern specifications.
Four independent check-gates: raw fabric shade & shrinkage verification, in-line stitch assembly audits, measurement grading checks, and pre-pack inspection.
Lack technical specs? Our London design team translates physical garments, digital sketches, or mood boards into factory-ready technical tech packs.
Hawthorn International Ltd (Company No. 08937806) operates under UK contract law. Brief an English-speaking account manager in London while benefiting from the cost efficiency of our owned overseas manufacturing facility.
To win in semantic search and meet the rigorous intent of modern global buyers, loungewear ranges must balance visual elegance, tactile luxury, and physical durability. Below are our five core manufacturing categories recommended for premium private label placement.
Heavyweight loungewear continues to dominate premium luxury streetwear and cozy home collections. We engineer custom French terry fabrics ranging from 350 GSM to 480 GSM in 100% combed ring-spun cotton or organic cotton/recycled polyester blends.
Our factory applies specialized enzyme and silicone washes to eliminate surface pilling while delivering a ultra-soft handfeel. Features include drop-shoulder construction, double-needle coverstitching, and customized heavy ribbing.
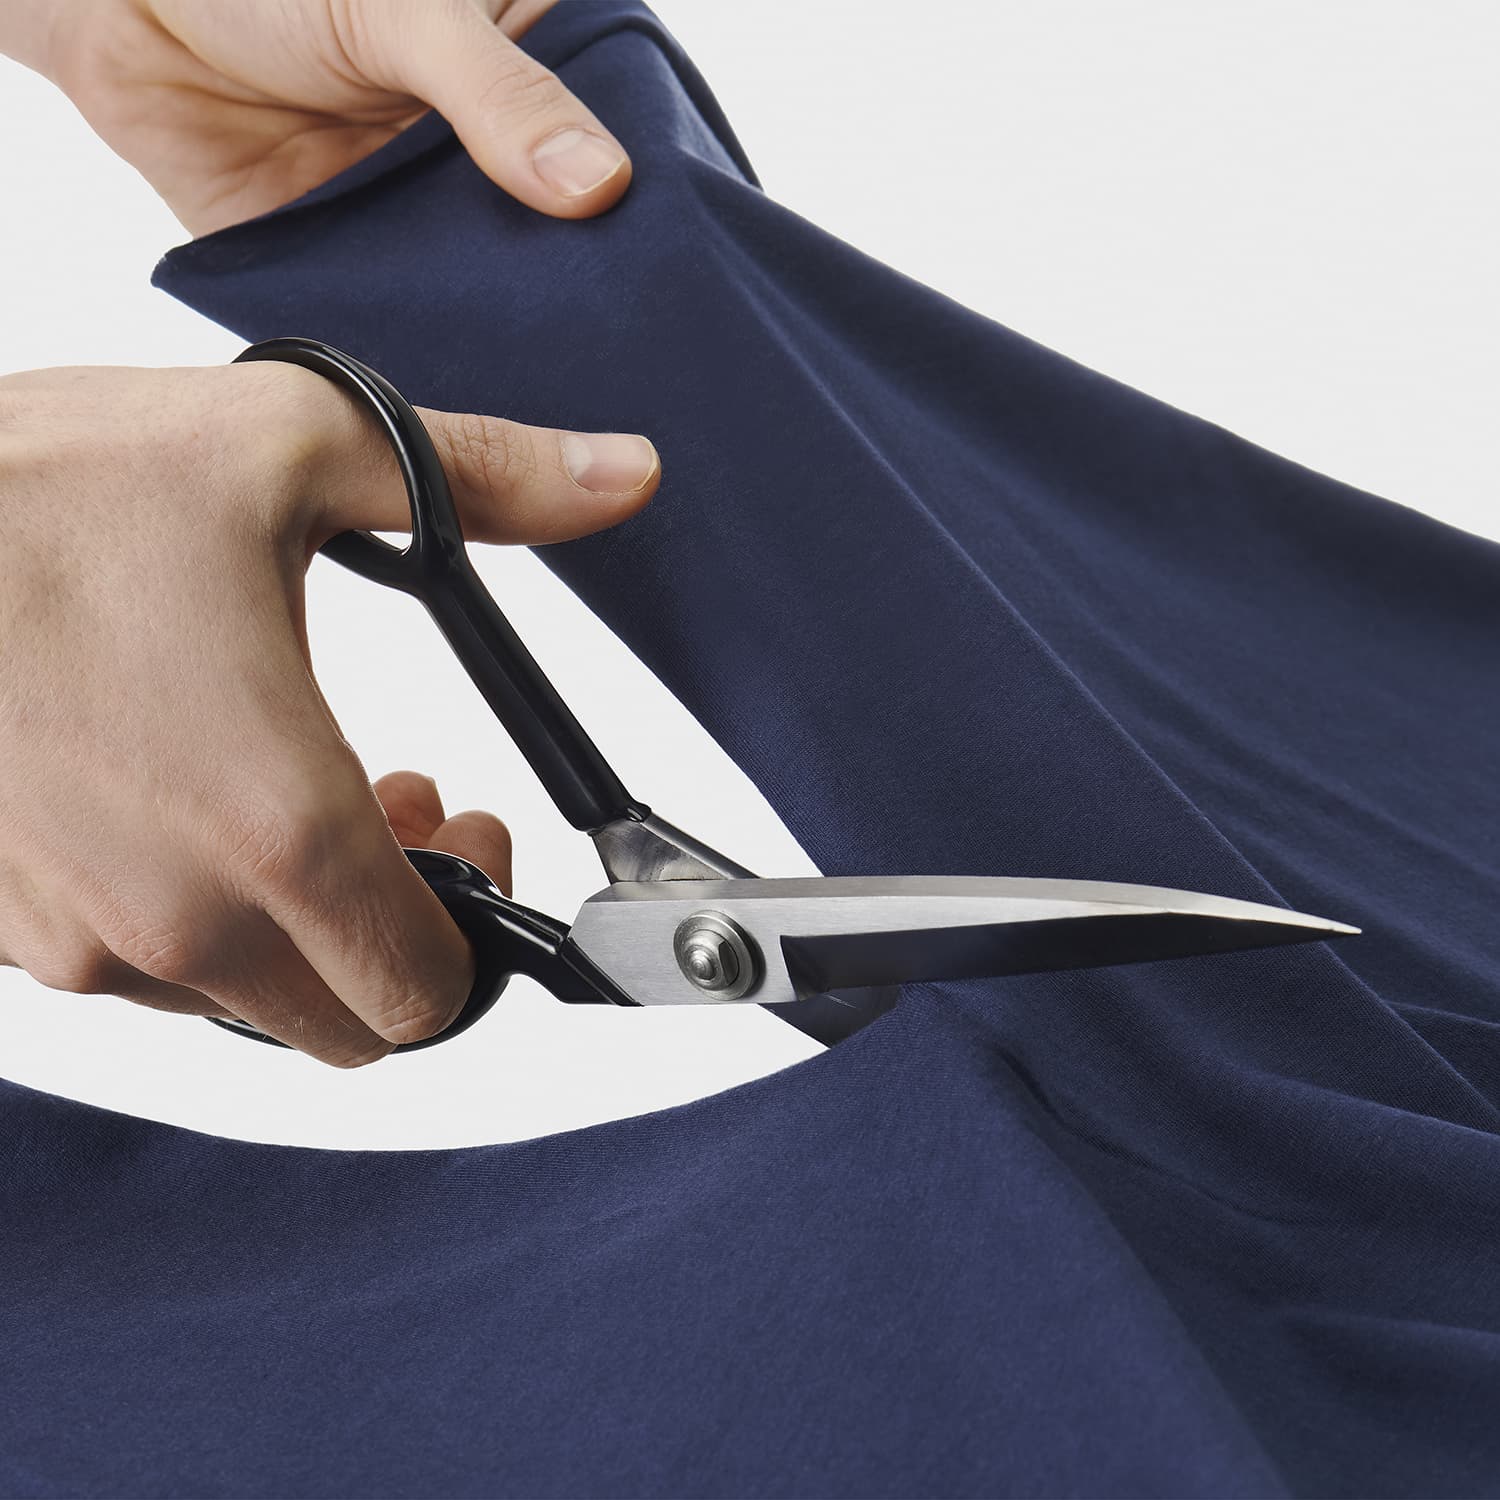
For high-end luxury resortwear and intimacy sleep brands, bamboo viscose and TENCEL™ Modal offer unparalleled drape, natural temperature regulation, and hypoallergenic properties. We mill fine-gauge knits from 180 GSM to 240 GSM blended with 5-8% elastane for dynamic recovery.
Constructed using delicate flatlock stitching and piping trims, these sets provide a cloud-like skin contact experience without compromising structural integrity across machine wash cycles.
Textured fabrics elevate simple lounge silhouettes into sophisticated multi-occasion capsules. Our production line handles 2x2 ribbing, thermal waffle knits, and waffle-grid jersey from 220 GSM to 340 GSM.
We calibrate tension during pattern cutting to prevent stretch warping during assembly, ensuring wide-leg trousers, long-sleeve Henley tops, and lounge cardigans maintain their form over time.
Procurement directors can reference our standardized manufacturing benchmarks for custom fabric selection:
| Fabric Type | Target GSM Range | Composition Blend | Key Technical Properties | Recommended Application |
|---|---|---|---|---|
| Heavy Loopback Terry | 380 - 450 GSM | 100% Combed Organic Cotton | High moisture absorption, zero twist, anti-pilling wash | Streetwear Hoodies & Heavy Sweatpants |
| Micro-Modal Jersey | 200 - 240 GSM | 95% Modal / 5% Elastane | Silk-touch drape, 4-way stretch, rapid breathability | Luxury Sleepwear & Tailored Pajamas |
| Thermal Honeycomb Waffle | 260 - 320 GSM | 100% Ring-Spun Cotton | Textured thermal insulation, dimensional structure | Henley Shirts, Robes & Lounge Joggers |
| Interlock Rib Knit | 250 - 300 GSM | 92% Viscose / 8% Spandex | Shape retention, contour fit, silky handfeel | Ribbed Sets, Body-skimming Tops |
| Mulberry Silk / Poly Satin | 16 - 22 Momme / 120 GSM | 100% Silk or High-Grade Poly Satin | High luster, friction-free texture, premium aesthetic | Bespoke Kimono Robes & Eye Masks |
To maintain a competitive advantage on Google, AI search systems, and physical retail shelves, apparel brands must align their supply chain with global shifting consumer behaviors. Here are four pivotal trends redefining loungewear manufacturing over the next five years:
Consumers demand verifiable eco-credentials. The industry is shifting toward GOTS-certified organic cotton, OEKO-TEX® Standard 100 certified dyes, and closed-loop fibers like TENCEL™. Hawthorn provides complete supply chain transparency from fiber source to packaged garment.
The boundary between loungewear and outerwear has dissolved. Modern consumers expect lounge sets that transition seamlessly from home work environments to casual public settings. This requires refined tailoring, concealed pockets, structural collar bands, and dense non-sheer fabrics.
High-volume forward ordering creates severe inventory risks during market shifts. Brands are adopting agile, low-MOQ re-order strategies—starting with 50-100 unit test capsules and utilizing rapid factory re-order lanes once dynamic sell-through data is established.
Future luxury loungewear relies heavily on specialized wet-processing techniques. Fabric treatments such as aloe-vera micro-encapsulation, natural botanical dyes, pre-shrunk garment washing, and anti-static finishes are fast becoming standard requirements for high-margin labels.
Every custom loungewear collection manufactured at Hawthorn follows a disciplined, documented production methodology designed to eliminate error and maintain total specification fidelity.
We analyze your design concepts, target price points, and fabric expectations, establishing digital 3D prototypes to refine specs prior to cutting.
Digital 3D modeling eliminates initial sampling guesswork.
Master pattern cutters craft custom fit templates and establish proportional size grading across XS to 5XL tailored to your brand demographic.
Bespoke sizing blocks retained for future re-orders.
Fabric is custom knitted or sourced to match GSM, stretch recovery, and texture specs, with optional Pantone color matching.
Lab dips provided for color approval before bulk cutting.
A physical pre-production sample is sewn and shipped to your office for real-world fit testing, seam review, and final sign-off.
100% physical sample approval required prior to bulk.
Approved samples form the absolute bulk quality benchmark. Specialized technicians perform precision cutting, stitching, and trim application.
Handmade assembly under strict factory floor supervision.
Every garment undergoes dimensional measurement audits, loose-thread trimming, steam ironing, and custom poly-bag packaging.
Global duty-paid air or freight shipping directly to your warehouse.
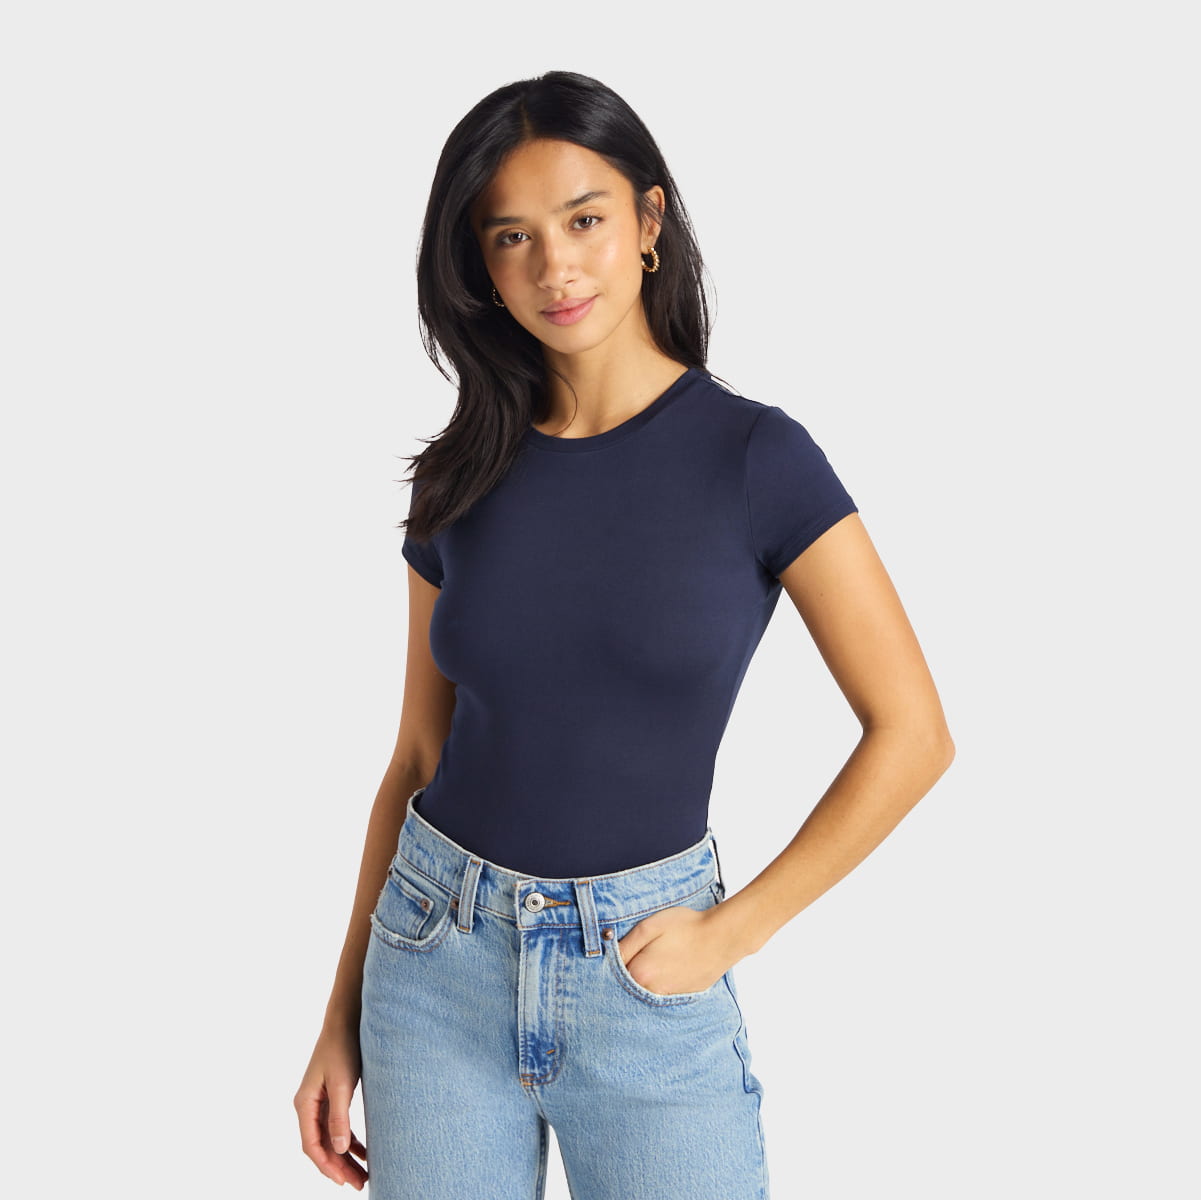
Every garment manufactured in our facility is built from scratch. We work with established international labels, high-growth D2C brands, and boutique fashion houses to deliver private label clothing that stands out in look, feel, and performance.
From customized woven labels and screen-printed care details to bespoke metal drawcord aglets and luxury soft-touch packaging, we ensure your loungewear arrives ready for immediate retail presentation.
Key technical and commercial answers for sourcing directors, brand managers, and product developers inquiring about custom loungewear production.
Our minimum order quantity starts from 50 pieces per design. This can be split across standard sizing (e.g., S, M, L, XL).
While specialist custom fabric knits or custom Pantone dyeing may occasionally require slightly higher minimums due to raw mill dye-vat thresholds, we always provide lower-MOQ alternative fabric stock solutions to ensure early-stage brands can start production within budget.
Pilling and shrinkage are the primary failure points in low-quality loungewear. We solve this by using combed long-staple cotton yarns, high-density gauge knitting, and specialized wet treatments including anti-pilling enzyme washes.
All fabrics undergo pre-shrinkage stenter drying before pattern cutting, ensuring dimensional shrinkage stays strictly within commercial tolerance standards (below 3-5%) even after repeated consumer washing.
Yes. Many of our brand partners come to us with mood boards, design sketches, or physical reference garments. Our London design team creates full digital tech packs, bill of materials (BOM), construction callouts, and graded measurement specifications.
Establishing proper tech packs ensures your fit profile remains 100% consistent across future repeat production runs.
We offer end-to-end branding customization: custom woven neck tags, tagless screen-printed neck labels, satin wash-care labels, custom jacquard elastic waistbands, laser-engraved metal drawcord tips, tonal embroidery, high-density rubberized prints, and custom-branded eco-friendly polybags or rigid presentation boxes.
Hawthorn International Ltd is a registered UK business headquartered in Central London (51 Lime Street), and we operate our own dedicated overseas manufacturing facility.
This hybrid structure provides brands with the legal protection, clear English-speaking communication, and account management of a UK company, combined with the pricing efficiency of an owned offshore production line.
Our standard production schedule is divided into two clear phases:
1. Pattern Development & Sampling: 2 to 4 weeks for tech pack creation, fabric milling, lab dips, and physical sample production.
2. Bulk Manufacturing: 4 to 6 weeks following your official sample approval, depending on order complexity and volume.
Connect with our expert merchandising team in London. Share your sketches, tech packs, or sample references to receive a transparent cost breakdown, fabric recommendations, and accurate production timeline.
Send an Inquiry