Explore our pre-developed technical blocks and custom cut-and-sew options, manufactured to order with strict quality thresholds.
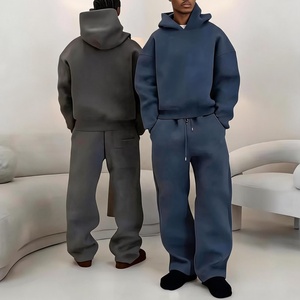
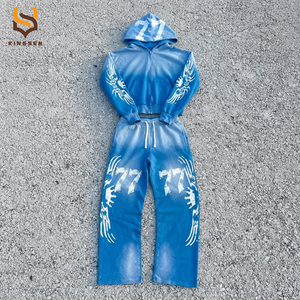
Bridging European account management accountability with direct, owned offshore manufacturing power.
Unlike middleman sourcing brokers or traditional third-party agents, Hawthorn maintains a corporate head office in Central London paired with directly owned, state-of-the-art offshore production facilities. Brands receive UK legal protections, clear English-language merchandising, and direct factory-floor pricing.
Capital preservation is essential for emerging athletic fashion houses. We offer low minimum order quantities starting from 50 pieces per design, allowing brands to test complex capsule drops, refine market fit, and scale volume iteratively without locking equity in warehouse overstock.
Defects are eliminated before garments reach packaging. Our standardized 4-stage quality control protocol ensures strict physical and dimensional compliance against your approved tech pack spec sheet at every stage of production.
In the contemporary athletic apparel ecosystem, consumer expectations have shifted dramatically from basic aesthetics to verifiable technical performance. A CE Certified Custom Activewear Manufacturer provides fashion brands, athletic teams, and enterprise distributors with the regulatory foundation needed to commercialize active apparel across international jurisdictions, particularly within the European Economic Area (EEA).
While standard athleisure apparel often bypasses rigorous regulatory scrutiny, specialized high-performance sportswear—such as protective compression wear, thermal outerwear, equine riding apparel, cycling armor, and UV-resistant outdoor activewear—falls directly under international safety standards. Under European Union Regulation (EU) 2016/425 governing Personal Protective Equipment (PPE), garments designed to protect against environmental extremes, friction impact, or mechanical stress must achieve formal CE certification.
As an authoritative OEM/ODM factory, our manufacturing processes integrate strict alignment with standard international testing measures:
Superior custom activewear starts at the polymer level. Our fabric development lab formulates bespoke circular knit and woven textiles tailored to specific athletic disciplines. Synthetic fibers such as Micro-Polyamide 6.6 (Nylon) and High-Multi Filament Polyester are co-knitted with Premium Elastane (Spandex/Lycra) to achieve high dynamic modulus recovery, ensuring garments retain structural shape after thousands of extension cycles.
Furthermore, advanced surface finishes are applied during jet-dyeing, including silver-ion antimicrobial treatments for odor control, hydrophilic capillary moisture-wicking coatings, and fluorocarbon-free durable water repellency (DWR). By integrating custom Pantone dyeing at the fabric mill stage, we ensure precise shade consistency across multi-season collections.
Garment longevity depends on seam integrity. Standard lockstitch seams often rupture under active elongation. Our production line utilizes specialized flatlock (four-needle, six-thread) stitching machinery, ultrasonic edge welding, and bonded thermo-film seam taping. Flatlock seam technology creates flat, chafe-free interior joins that lay flush against athlete skin, enhancing hydrodynamic efficiency and preventing mechanical abrasion during intense exercise routines.
Navigating upcoming technological shifts, regulatory mandates, and supply chain transformations over the next decade.
The global regulatory climate is mandating a shift away from virgin petroleum-based synthetics. Sourcing strategies are prioritizing GRS-certified (Global Recycled Standard) Recycled Nylon (Econyl), post-consumer rPET, and bio-based polyesters derived from plant lipids. Future activewear lines will require monomer-level recyclable mono-material construction to comply with emerging extended producer responsibility (EPR) legislation.
Physical sample iterations waste capital, time, and fabric resources. Sourcing workflows are shifting to 3D CAD simulations (Clo3D, Browzwear). By testing digital twin apparel on dynamic avatars, pattern draping, strain maps, and tension points are evaluated virtually. This slashes pre-production sample lead times from 4 weeks down to several business days while reducing waste.
Geopolitical turbulence and high shipping costs are reshaping sourcing models. Forward-thinking apparel brands are abandoning rigid, high-volume single-location models in favor of hybrid agile supply networks. By pairing centralized digital pattern creation with regionalized flexible manufacturing facilities, brands maintain short-run agility without ballooning unit costs.
Activewear development has evolved beyond basic casual cotton-poly blend sweatsuits into highly engineered apparel requiring specialized manufacturing equipment. Understanding this trajectory allows brand owners to properly position their product lines for maximum commercial margin.
Historically, sportswear consisted mainly of heavyweight cotton fleeces, basic jersey crewnecks, and loose-fitting track jackets. Manufacturing focused on structural durability, heavy GSM weights (300GSM–500GSM), and basic screen printing. While this market segment remains strong within custom streetwear drops, modern performance brands require far higher technical capabilities.
The rise of specialized gym apparel introduced seamless circular knitting (Santoni machines), mapping body contours directly into variable-density knit patterns. High-compression garments utilize targeted elasticity zones to assist venous return, stabilize muscle groups during explosive lifts, and reduce micro-trauma fatigue. Producing these items requires high-precision circular knitting capabilities alongside skilled manual assembly for edge trim binding.
The current state-of-the-art in custom activewear manufacturing fuses technical knits with functional hybrid features: laser-cut ventilation zones, bonded waterproof pockets, 3M reflective element placement, micro-encapsulated phase-change thermal regulation materials, and conductive smart-yarn sensor integration. Partnering with an experienced factory ensures these advanced elements are applied reliably across bulk production runs.
Transparent responses to key questions raised by sourcing directors and brand founders.
Partner with an established, CE-compliant technical garment manufacturer. Speak with our UK account management team today to review your designs, tech packs, or reference samples.
Contact Us