Engineered for high-street retail, private label scaling, and heavy-duty activewear drops. Minimum order quantity starting from 50 pcs/design.
An authoritative guide for fashion startups, SMEs, and enterprise brands on compliance benchmarking, low-MOQ procurement, and zero-defect manufacturing engineering.
In the modern global apparel matrix, CE Certification (Conformité Européenne) and adherence to EU Regulation 2016/425, REACH chemistry bounds, and OEKO-TEX Standard 100 are no longer optional compliance badges—they represent the bedrock of brand protection and consumer trust. When importing wholesale activewear, streetwear, and technical hoodies into European and North American territories, importers must ensure that raw materials, AZO dyes, heavy metal thresholds, and physical construction meet strict regulatory safety standards.
Hawthorn International bridges the critical gap between stringent European regulatory oversight and cost-effective offshore production lines. By establishing a dual-hub framework—headquartered in Central London, UK, with owned direct-manufacturing facilities overseas—we eliminate third-party agency markups while implementing rigid British quality management systems (QMS) directly on the factory floor.
Combining UK contract security and dedicated English-speaking account directors with direct-owned manufacturing cost efficiency.
Traditional apparel factories demand 500 to 1,000 units per colorway, locking up vital brand capital in unsold inventory. Our flexible assembly lines allow brands to launch capsule collections starting at just 50 pieces per design. Test your fit market, establish proof-of-demand, and scale seamlessly into 5,000-unit bulk reorders without re-tooling your pattern blocks.
Defects are eliminated before shipping. We execute incoming fabric inspections, in-line stitching audits, end-of-line dimension measuring against your size chart, and a final pre-pack AQL 2.5 audit.
Don't have a finished tech pack? Our in-house pattern masters translate physical samples, hand sketches, or digital moodboards into standardized CAD files, grading tables, and complete Bills of Materials (BOM).
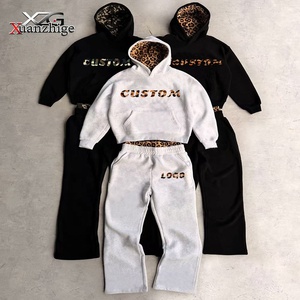
We build every garment cut-and-sew from ground zero. Take total artistic control over fabric weight (280GSM to 500GSM heavyweight cottons), custom ribbing weave, high-density embroidery, screen printing, 3D silicone badges, custom YKK hardware, and exact Pantone color matching at mill level.
Key market shifts altering the global B2B apparel export landscape and how wholesale buyers can optimize margin vulnerability.
Wholesale buyers are aggressively moving away from legacy 6-month buying cycles toward 4-to-6-week agile replenishment models. By maintaining low-MOQ baseline patterns with custom mills, brands reduce dead-stock risk by up to 64%, utilizing real-time sales telemetry to trigger automated reorders.
European Digital Product Passport (DPP) regulations mandate complete material traceability. Future-ready exporters are embedding GOTS-certified organic cottons, GRS-recycled polyesters, and waterless ozone wash techniques into standard production streams without compromising luxury handfeel.
Physical sample iterations historically consumed 30% of pre-production time. By implementing CLO3D and Browzwear digital twin prototyping, garment drape, tension maps, and print placements are verified digitally, trimming prototype approval turnarounds from 28 days down to 5 days.
Streetwear consumers now prioritize structural drape over flimsy blends. Demand for ultra-heavyweight fabrics (400GSM to 550GSM loopback French Terry and double-faced tech fleece) has grown by 180% year-over-year, requiring high-density needle looms during manufacturing.
Understanding technical fabrication methods to optimize product positioning and consumer retail price points.
| Manufacturing Technique | Ideal Product Category | Technical Characteristics | Durability Rating | CE & Compliance Status |
|---|---|---|---|---|
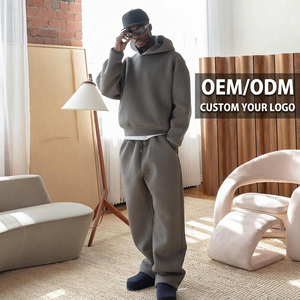
| Heavyweight French Terry (400+ GSM) | Oversized Hoodies & Baggy Sweatpants | 100% Combed Cotton, zero-bleed reactive dyeing, high structural drape. | Ultra High (100+ Washes) | Fully REACH & OEKO-TEX Passed |
| Enzyme & Acid Wash Finishing | Vintage Streetwear & Tracksuits | Custom chemical wash neutralizing alkalinity, soft handfeel, pre-shrunk. | High (Pre-Shrunk) | Neutralized pH (ISO 3071) |
| 3M Scotchlite™ Reflective Bonding | Windbreakers & Tech Joggers | Glass bead retroreflective technology heat-sealed onto nylon matrix. | ISO 20471 Certified | CE EN 17353 Compliant |
| Thermal Tech Fleece Bonding | Winter Athletic Tracksuits | Double-knit synthetic/cotton face with micro-fleece insulating backing. | High Thermal Efficiency | Class 1 Fire Safety Tested |
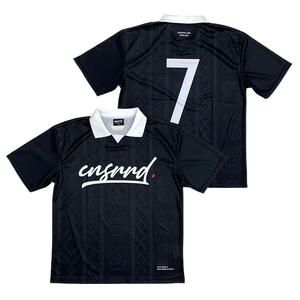
| Automated Sublimation Printing | Retro Soccer Jerseys & Kits | Direct dye-dispersion into polyester fibers; zero cracking or peeling. | Permanent Color Fixation | AZO-Free Inks Standard |
How your custom clothing order progresses from initial concept sketch to certified delivery.
We audit your design specifications, build CAD tech packs, define garment measurements, and establish target unit pricing.
Master tailors create individual sizing blocks across XS to 3XL, ensuring proportional fit consistency across the entire size curve.
Yarn is knitted or woven to your exact composition, GSM weight, and handfeel specifications, accompanied by custom Pantone color dyeing.
A complete pre-production sample is stitched, branded, and dispatched to your office for physical evaluation and sign-off.
Upon sample approval, automated laser cutters and skilled sewing operators assemble your bulk order on our dedicated assembly line.
Every garment passes 4-stage quality checks, individually polybagged with custom hangtags, and shipped directly via DHL/FedEx/Freight.
Everything you need to know about lead times, certifications, tech pack requirements, and customs logistics.
CE Certification verifies that garments meet European Union safety, health, and environmental protection standards. For apparel exporters, this ensures raw fabrics are free from prohibited chemical AZO dyes, comply with REACH safety parameters, and feature fire safety compliance for fleece and technical activewear.
Our minimum order quantity starts from just 50 pieces per design. You can split this MOQ across standard size runs (e.g., S, M, L, XL). For complex Pantone-dyed fabrics or custom-knitted Jacquard textiles, fabric mill minimums may apply, which our team will transparently outline up front.
We specialize in 100% custom cut-and-sew manufacturing. We do not re-sell pre-made catalog blanks. Every panel is cut, dyed, printed, stitched, and custom-labeled specifically for your brand order, ensuring true unique market differentiation.
Pattern creation and physical prototype sampling generally take 2 to 4 weeks. Once the sample is approved, bulk production takes approximately 4 to 6 weeks, depending on fabric dye cycles and order complexity.
No problem. You can provide physical reference samples, dimensional notes, or high-resolution graphic mockups. Our in-house technical fashion designers will generate a complete production-ready tech pack, grading chart, and bill of materials for your approval.
We implement a strict 4-Stage Quality Control Protocol: raw fabric inspection, in-line seam checking, end-of-line dimension audits against approved tech pack tolerances, and a final pre-shipment AQL 2.5 audit prior to carton sealing.
Connect directly with our UK account team. Submit your tech pack, sketches, or design ideas for an immediate quote, low MOQ confirmation, and production timeline assessment.
Contact Us