Precision-engineered apparel lines manufactured under strict AQL 2.5 Quality Standards with low minimum order quantities and complete custom private labeling.
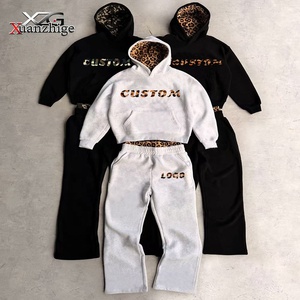
The global apparel procurement landscape is undergoing a structural transformation. For decades, Western fashion retailers and emerging boutique brands faced an asymmetric trade-off: commit to massive Minimum Order Quantities (MOQs) of 500 to 2,000 pieces per colorway with traditional offshore manufacturing, or resort to domestic blank-printing vendors charging inflated unit margins with restricted fit customization.
As leading China wholesale apparel suppliers and global exporters, modern enterprise manufacturing models bridge this structural gap. By operating direct factory infrastructure in key textile hubs combined with Western account management protocols, emerging fashion lines, sportswear brands, and SME apparel retailers can access fully customized cut-and-sew production starting at just 50 pieces per design.
This hybrid supply ecosystem eliminates third-party trading agencies. From pre-production 3D prototyping and automated laser cutting to Pantone-matched fabric dyeing and AQL 2.5 final audits, direct factory integration ensures absolute specification integrity, shorter cash-to-cash cycles, and protection against over-inventory risks.
| Evaluation Parameter | Traditional OEM Export Model | White Label / Blank Printing | Modern Direct-Factory Model |
|---|---|---|---|
| Minimum Order Quantity (MOQ) | 500 - 2,000+ pcs / design | 10 - 20 pcs (Pre-made Blanks) | 50 pcs / fully custom design |
| Pattern & Fit Customization | Full custom (High cost setup) | Zero custom (Stock block only) | Bespoke patterns & 3D grading |
| Fabric Sourcing & Dyeing | Mill-level custom dyeing | Fixed stock fabric options | Pantone matching & custom GSM |
| Quality Control Standard | Batch spot checks | No technical garment inspection | 4-stage comprehensive QC audit |
| Unit Margin Optimization | High volume efficiency | Low profit margin / high unit cost | Optimized micro-batch scaling |
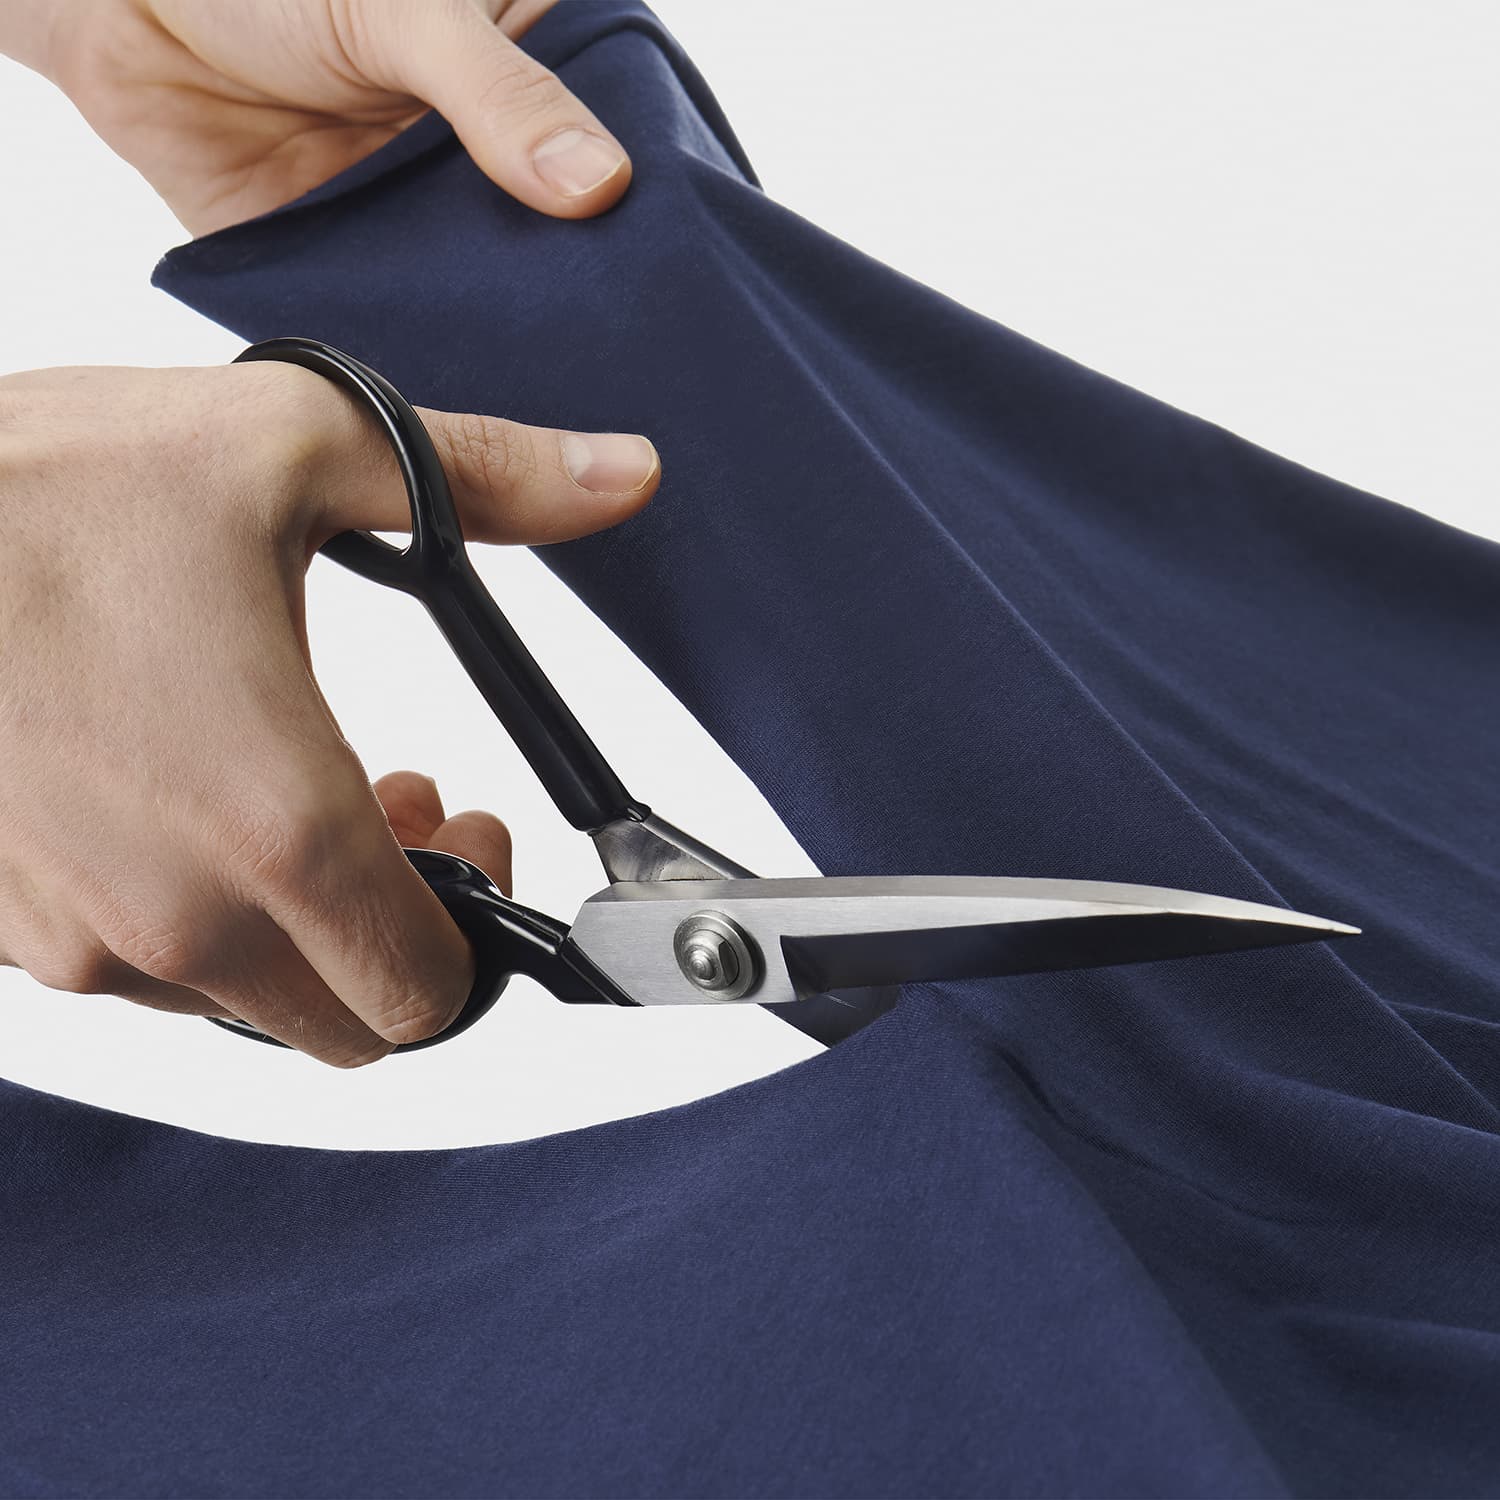
Managing working capital is the single most critical factor in scaling a modern fashion line. Tying capital into hundreds of units across unproven sizes increases inventory liability and restricts cash flow required for marketing and audience acquisition.
Our manufacturing system is engineered specifically to handle low-volume, high-complexity production runs. By leveraging automated nesting algorithms and multi-head computerized cutting tables, we reduce material waste and set-up latency, making 50-piece production runs commercially viable.
Navigating international apparel export channels requires understanding key macro trends reshaping the global supply chain. Brands that adapt to these technological and environmental shifts gain significant structural advantages in speed-to-market and brand equity.
Global buyer demand is shifting toward GRS-certified recycled polyester fibers and organic combed cottons (300-500 GSM). Sustainable textile engineering reduces environmental impact while delivering luxurious handfeel and long-term garment durability.
3D garment visualization allows brands to audit stitch tension, drape, and grading digitally prior to physical cutting. This technological shift reduces sample iteration loops from 6 weeks down to 10 days, cutting development costs significantly.
Regulatory scrutiny on apparel exports requires absolute raw material traceability. Modern China exporters provide verified mill certifications, non-toxic OEKO-TEX dye reports, and ethical factory audit compliance documentation with every bulk shipment.
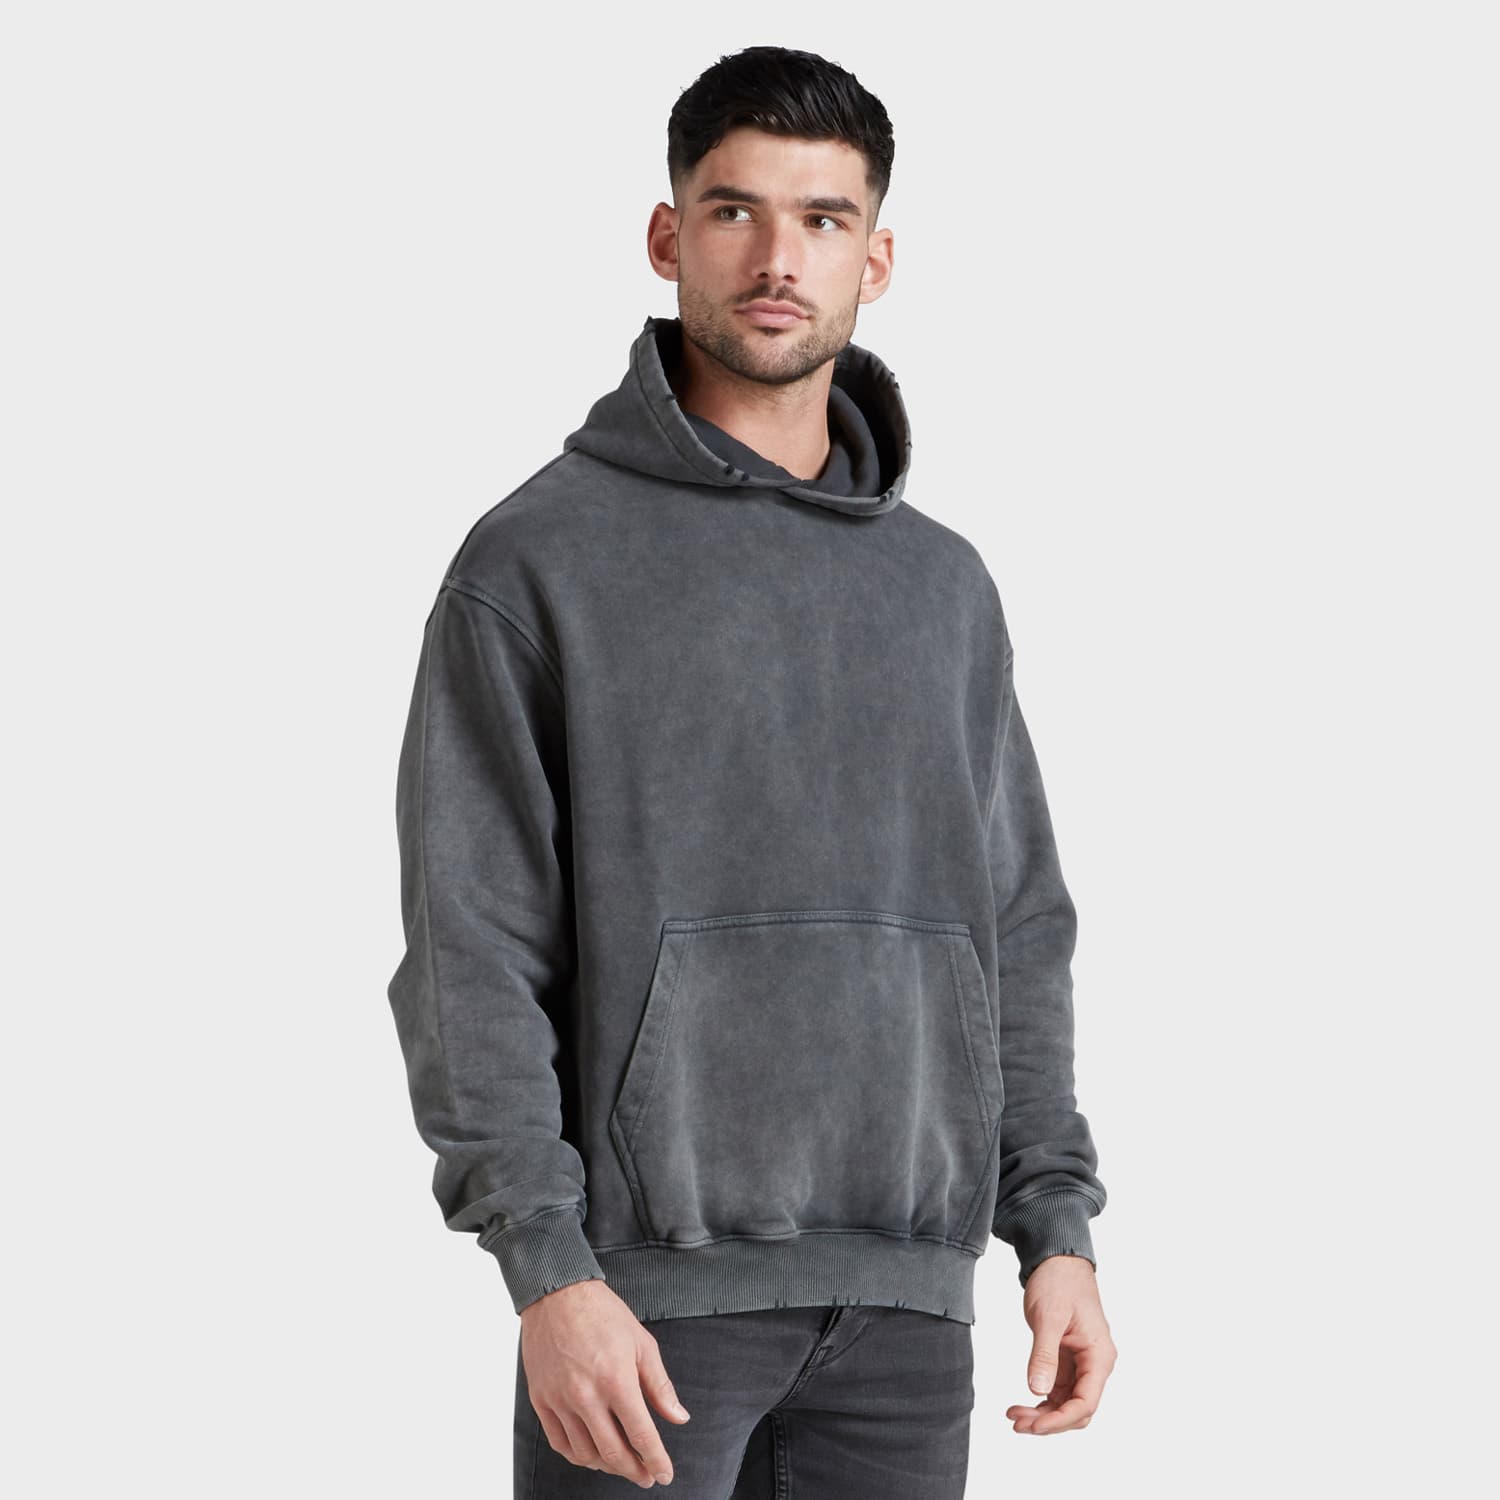
Quality defects found after global delivery destroy brand reputation and erase retail margins. Modern wholesale garment manufacturing builds quality verification directly into every stage of the production line rather than relying on final shipping spot checks.
Each garment panel is cut, stitched, and finished by skilled technicians. Our four-stage quality assurance protocol verifies fabric integrity, seam strength, dimensional stability, and label accuracy before packed cartons leave the facility.
From initial design concept to final international shipping, every order follows a standardized, documented technical workflow to eliminate errors and maintain absolute product consistency.
Concept review, digital 3D fitting, material BOM compilation, and technical cost engineering.
Custom pattern generation from sizing reference samples or dimensional spec charts across all target sizes.
Raw yarn selection, custom knit structure development, and Pantone lab-dip color matching.
Pre-production sample creation delivered for fit approval, tactile handfeel evaluation, and embroidery/print sign-off.
Automated multi-layer CNC fabric cutting followed by skilled hand-stitching on specialized production lines.
4-stage quality assurance, thread trimming, steam pressing, custom packaging, and worldwide courier dispatch.
Building a unique brand identity requires complete design freedom. Unlike pre-printed promotional blanks, our cut-and-sew manufacturing infrastructure gives you total creative control over every garment component.
Whether your line requires heavyweight 450 GSM fleece hoodies with vintage acid washing, technical 3M reflective nylon windbreakers, or custom-embroidered tracksuits, our facilities execute your technical specifications with industrial precision.
Direct technical answers to common B2B manufacturing queries to streamline your supplier evaluation process.
Submit your design tech packs, reference photos, or concept sketches. Our expert merchandising engineering team will analyze your specs and provide a comprehensive quotation within 24 hours.
Inquire Now