
Top Trusted Bulk Apparel Supplier & Exporter

Precision Cut-and-Sew Garment Manufacturing, Low Minimums, and ISO-Compliant Global Export Solutions for Scale Brands

Featured Wholesale Collection

High-Demand Custom Garments & Blank Formats

Engineered for high-street retail, private label collections, and luxury streetwear capsules. Fully customizable with complete technical specs.

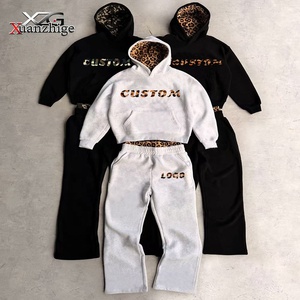
Custom High Quality Women's Custom Logo Leopard & Camo Lined 2-Piece Tracksuit

Custom High Quality Women's Custom Logo Leopard & Camo Lined 2-Piece Tracksuit, Oversized Crop Hoodie & Wide-Leg Jogger Set

Get a Quote
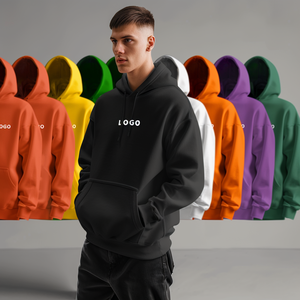
Custom Print 60% Cotton 40% Polyester Men's Hoodie Sweatshirt OEM

Custom Print 60% Cotton 40% Polyester Men's Hoodie Sweatshirt OEM Service High Quality Custom Fleece Black Hoodies Manufacturer

Get a Quote
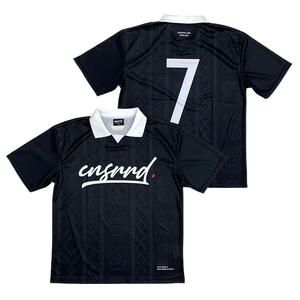
Retro Football Shirts Soccer Suits Vintage Custom Jerseys

Factory Direct Sales Retro Football Shirts Soccer Suits Vintage Custom Jerseys Soccer Tracksuit Sets Automated Cutting Unisex

Get a Quote
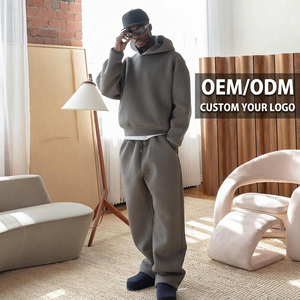
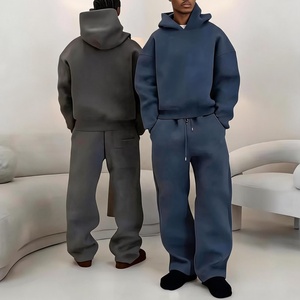
Heavy Weight Custom Winter Two Piece Baggy Sweatpants and Hoodie Set

Heavy Weight Custom Winter Two Piece Baggy Sweatpants and Hoodie Set Men Pullover Custom Oversized Hoodie Men Tracksuits

Get a Quote
Custom Lightweight Jogger Set 3m Reflective Windbreaker Sweatsuit

Custom Lightweight Jogger Set 3m Reflective Windbreaker Sweatsuit Nylon Tracksuit Nylon Windbreaker Jacket Sweatpants Set

Get a Quote
YITE Unisex Sweat Suits Heavyweight Cotton Blank Oversized Hoodies

YITE Unisex Sweat Suits Heavyweight Cotton Blank Oversized Hoodies and Sweatpants Sets Custom Logo Tech Fleece Men Tracksuit

Get a Quote
ARTISAN High Quality Wholesale Blank Custom Tracksuit Men

ARTISAN High Quality Wholesale Blank Custom Tracksuit Men Fashion Streetwear Men's 2 Piece Cropped Zip up Tracksuit Sweatsuit

Get a Quote
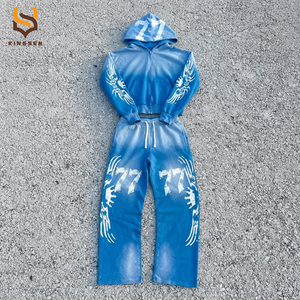
Custom Washed Sweat Suit Zipper Hoodies Tracksuit Set Printing Acid Wash

Custom Washed Sweat Suit Zipper Hoodies Tracksuit Set Printing Acid Wash Flared Sweatpants And Hoodie Set

Get a Quote
50 Pcs
Low Starting MOQ
2,000+
Global Brands Scaled
4-Stage
ISO Quality Control
10+ Yrs
Manufacturing Expertise
Technical Whitepaper

Re-engineering Bulk Apparel Sourcing: Precision, Agility & E-E-A-T Quality

An authoritative analysis of global garment export mechanics, fabric weight dynamics, and tech-pack optimization for modern apparel buyers.

1. Strategic Shifts in Global Garment Procurement

In the evolving ecosystem of global fashion supply chains, procurement directors and apparel entrepreneurs face a structural dilemma: balancing high capital commitment against demand unpredictability. Traditional overseas apparel manufacturers historically demanded Minimum Order Quantities (MOQs) exceeding 1,000 to 5,000 pieces per colorway. This legacy framework forced emerging labels, direct-to-consumer (DTC) powerhouses, and boutique apparel brands to over-index capital into speculative inventory, leading to heavy discounting or deadstock write-offs.

As a leading UK-headquartered bulk apparel supplier with owned offshore manufacturing facilities, Hawthorn International bridges the operational gap between Western commercial accountability and offshore production economics. Operating under central management based in London alongside dedicated account merchandisers, we remove traditional intermediary agents, providing direct access to cut-and-sew lines while enforcing strict UK legal and quality standards across all production orders.

Key Procurement Insight: Small-batch agility (starting at 50 pieces per design) combined with standardized technical grading reduces initial inventory carry costs by up to 68%, enabling brands to test localized consumer cohorts prior to committing to high-volume bulk runs.

2. Material Science & Fabric Weight (GSM) Optimization

Evaluating bulk apparel quality requires a granular understanding of textile physics, yarn count, and fabric grammage (GSM — grams per square meter). High-end streetwear, technical athletic wear, and premium loungewear rely heavily on exact yarn blends to maintain structural drape, hand-feel, and longevity after repeated wash cycles.

When sourcing heavyweight fleece hoodies or tracksuits, cotton-to-polyester ratio directly governs thermal efficiency, breathability, and shrinkage parameters:

  • Heavyweight Fleece (380 GSM – 500 GSM): Typically constructed from a 100% combed cotton or 80/20 CVC (Chief Value Cotton) face yarn. This dense French Terry or brushed fleece structure delivers the structural drop-shoulder profile favored by luxury streetwear labels while resisting surface pilling.
  • Performance CVC Blends (60% Cotton / 40% Polyester, 300 GSM – 350 GSM): Engineered specifically for daily wear tracksuits and active sets. Polyester reinforcement enhances tensile strength and colorfastness during high-temperature washing, while high cotton content guarantees moisture absorption and tactile softness against the skin.
  • Technical Synthetics & Nylon Fabrics (110 GSM – 180 GSM): Utilized in 3M reflective windbreakers and jogger sets. Micro-denier nylon weaves integrated with polyurethane (PU) back-coatings offer water repellency and windproofing without sacrificing breathability.

3. Pattern Engineering, 3D Prototyping & Tech Pack Integration

To eliminate discrepancies between initial sketches and mass production outputs, our technical design department utilizes advanced 3D CAD pattern modeling and automated marker making. A tech pack serves as the immutable single source of truth for garment construction. Every measurement tolerance, seam construction type (e.g., flatlock stitching, double-needle coverstitching, bar-tacking at stress points), stitch-per-inch (SPI) rating, and trim bill of materials (BOM) is validated during pre-production sampling.

Brands lacking complete technical tech packs can leverage our full-service design team. By evaluating physical reference garments, tech packs are synthesized to lock in shoulder slants, sleeve crowns, hood curvatures, and waist-to-hip grading scales across XS through 3XL sizing.

Corporate Superiority

Why Enterprise & Start-Up Brands Partner With Us

Built upon transparent UK account management, proprietary manufacturing assets, and unyielding quality governance.

Low MOQ Flexibility (50 Pcs)

Launch targeted capsules without massive capital outlays. Our flexible production lines allow custom cut-and-sew manufacturing from just 50 pieces per design, scalable to tens of thousands.

4-Stage Quality Assurance

Every garment undergoes incoming fabric shade/defect inspection, in-line seam checks, end-of-line dimensional audits, and a final pre-pack quality control review before global export.

Direct Factory Ownership

We own and operate our offshore garment factory. You gain foreign factory pricing coupled with London head office communication, transparent timelines, and UK legal security.

Bespoke Customization & Dyeing

Pantone color matching, acid washing, enzyme washing, high-density screen printing, 3D puff embroidery, and custom 3M reflective applications executed under one roof.

Automated Precision Cutting

Using computerized multi-ply laser and knife cutters, panel dimensions are accurate within sub-millimeter tolerances, ensuring identical fit across all production batches.

End-to-End Export Logistics

Seamless door-to-door global shipping, automated customs documentation, land/sea/air freight optimization, and DDP (Delivered Duty Paid) fulfillment options worldwide.

Market Forecasting

Future Apparel Procurement Trends & Innovations

Navigating the global textile ecosystem: What procurement teams must prepare for between 2025 and 2030.

1. Eco-Conscious Synthetics & Closed-Loop Sustainable Cotton

Global regulatory frameworks (such as the EU Corporate Sustainability Due Diligence Directive and digital product passport mandates) are rapidly transforming garment importing rules. Brands can no longer rely on unverified raw material claims. The future of bulk apparel export centers on certified traceable inputs: GOTS-certified (Global Organic Textile Standard) organic cotton, GRS-certified (Global Recycled Standard) recycled polyester derived from post-consumer PET bottles, and eco-friendly non-toxic reactive dyes.

Our manufacturing lines integrate low-liquor-ratio dyeing machinery that reduces water consumption by up to 45% compared to traditional exhaust dyeing systems. Furthermore, recycled fleece blends now achieve identical tensile strength, brush softness, and wash durability as virgin synthetic polymers, meeting consumer demand for sustainable apparel without compromising luxury hand-feel.

2. Special Effects: Acid Wash, Pigment Dyeing & Technical Trims

Vintage streetwear aesthetics—characterized by sun-faded treatments, acid washes, distress distressing, and mineral washes—require precise chemical stabilization to preserve garment structural integrity. Traditional wash houses often weaken fabric fibers, leading to tears around pocket corners and seams. Modern garment processing applies enzyme silicone washes post-construction alongside neutralized ozone treatments, achieving authentic retro patinas while retaining burst strength across fleece and jersey panels.

Simultaneously, functional safety features are merging into urban apparel. High-grade 3M Scotchlite reflective films and micro-prismatic heat-transfer membranes are embedded directly into nylon tracksuits and activewear, providing 360-degree night visibility for urban commuters and athletic users alike.

3. Nearshoring Governance with Offshore Production Efficiency

Supply chain shocks over recent years have forced fashion brands to rethink pure offshore broker models. The winning model for mid-sized apparel businesses is a hybrid strategy: Western-based account directors, tech-pack developers, and contracts working directly with owned overseas factory lines. This structure guarantees quick sampling cycles (2–3 weeks) and fast bulk production turnaround (4–6 weeks post-sample approval), giving brands the agility required to react swiftly to viral social commerce trends.

Frequently Asked Questions

Comprehensive Bulk Apparel Procurement FAQ

Direct technical and operational answers to address essential manufacturing questions before placing your order.

Where are Hawthorn's manufacturing facilities located and how is quality governed?

Hawthorn International Ltd operates under a dual-tier structure: our global corporate head office and senior account management team are based in Central London, UK (Company No. 08937806), while garment production takes place in our fully owned, purpose-built offshore manufacturing facility. This unique operational setup grants clients direct factory-floor pricing alongside UK commercial contracts, native English communication, and strict adherence to European/US garment compliance standards. Quality is governed by our on-site QC team using a 4-stage inspection protocol spanning raw material testing to final carton packing.

What is your true Minimum Order Quantity (MOQ) per design and colorway?

Our standard minimum order quantity starts from 50 pieces per design. This MOQ can be split across standard sizing runs (e.g., S, M, L, XL). Certain highly specialized technical specifications—such as custom-milled jacquard knits, custom Pantone fabric dyeing, or complex multi-panel outerwear—may require slightly higher minimums (100–300 pcs) due to raw textile mill minimums. If your design triggers a mill threshold, our merchandising team will immediately provide alternative in-stock fabric options to maintain your 50-piece target.

Do you offer stock blank clothing, or is every garment made-to-order?

We do not re-sell cheap pre-made white-label stock blanks. Every garment produced by Hawthorn is 100% custom cut-and-sewn from raw fabric rolls according to your specific tech pack, pattern cut, fabric composition, GSM weight, dye color, and branding parameters. For clients looking to accelerate development, we maintain a bank of pre-tested fit blocks (heavyweight hoodie cuts, wide-leg joggers, oversized drop-shoulder tees) that can be customized instantly with your chosen fabric, wash finish, graphics, and custom neck labels.

What are the standard lead times for prototyping, sampling, and bulk production?

As an accurate operational guide:

  • Pattern Cutting & Pre-Production Sampling: 2 to 4 weeks from tech pack finalization and fabric swatch sign-off.
  • Bulk Garment Manufacturing: 4 to 6 weeks following physical sample approval by your team.
  • Global Shipping & Transit: Air freight typically takes 5–8 business days door-to-door, while ocean freight ranges from 25–35 days depending on destination port.

What technical details must be included in a Tech Pack before requesting a quote?

While a full tech pack speeds up quotation, it is not mandatory to start. A complete tech pack should ideally contain: 2D vector flat sketches (front/back), detailed measurement specs across all sizes, desired fabric GSM and fiber composition, color Pantone numbers, artwork print/embroidery dimensions and placement, plus trim preferences (zips, drawcords, eyelets, labels). If you only possess rough sketches or physical reference garments, our internal apparel design team can generate a complete industrial tech pack and size chart on your behalf.

How does your 4-Stage Quality Control (QC) process function during bulk runs?

Defects are caught at the point of origin to guarantee consistency:

  • Stage 1 (Fabric Inspection): Raw fabric rolls are examined for color consistency, weight (GSM) accuracy, shrinkage potential, and surface defects before cutting.
  • Stage 2 (In-Line Stitching Audit): Quality engineers check needle tension, seam alignment, flatlock stability, and print positioning during assembly.
  • Stage 3 (End-of-Line Measurement): Assembled garments are measured against approved tech-pack size tolerance charts (+/- 0.5cm variance maximum).
  • Stage 4 (Final Pre-Pack Inspection): Garments undergo loose thread trimming, hardware functionality tests (zips/snaps), iron pressing, swing-tag checking, and polybag sealing.

Can you execute complex custom wash treatments like acid wash, vintage dye, or distress?

Yes. Our garment-dye facility specializes in advanced fashion treatments including acid washing, pigment wash, mineral fade, oil wash, tie-dye, stone washing, and hand-distressing. All vintage washes undergo chemical neutralization to ensure fabric ph-neutrality and structural longevity, preventing shrinkage post-purchase.

What branding options are available for private label apparel collections?

We deliver full turn-key branding solutions. Customization capabilities include woven damask neck labels, printed care labels, screen-printed interior sizing logos, custom embossed metal zip pulls, engraved eyelets, silicone or rubber patches, 3M reflective heat transfers, high-density puff printing, chenille patches, custom swing tags, and printed bio-degradable frosted polybags.

Ready to Manufacture Your Custom Garment Collection?

Partner with a trusted UK-managed bulk apparel supplier and exporter. Connect with our technical merchandising team today to discuss your specs, fabric requirements, and factory schedules.