Precision-engineered dyes, industrial dyeing machinery, and vintage-washed apparel engineered for low-MOQ brand scaling and custom tech-pack execution.
From SoMa tech-utility aesthetics to Haight-Ashbury vintage revivals, San Francisco brands require a unique blend of sustainable chemistry, low-inventory risks, and micro-climate versatility.
San Francisco’s iconic weather profile—characterized by rapid temperature swings between the Fog Belt and sunny Mission District microclimates—demands high-density heavyweight knits (380GSM to 500GSM french terry cotton and 280GSM ring-spun jerseys). Traditional piece-dyed fabrics often exhibit stiff hand-feels and uneven seam shrinkage under heavy moisture. Our custom OEM garment dyeing process treats fully constructed garments in specialized low-liquor ratio vats. This stress-relaxes the cotton fibers, pre-shrinks the apparel to sub-1% tolerances, and infuses an buttery ultra-soft hand-feel essential for Bay Area layering aesthetics.
Direct-to-Consumer (D2C) brands in Northern California face extreme inventory holding costs. By producing Prepared-For-Dyeing (PFD) raw inventory, SF brands can hold blank, un-dyed cut-and-sew apparel stock in reserve. When seasonal color trends shift, our OEM facility executes 14-day turnaround pigment or reactive garment dye drops, completely eliminating deadstock risk.
California apparel regulations (including strict water discharge standards and Proposition 65 chemical compliance) mean SF brands cannot risk working with non-compliant overseas mills. Our dye house utilizes eco-friendly disperse carriers, non-toxic direct dyes like Direct Black EX / 38, GOTS-certified organic pigments, and zero-discharge water filtration systems matching OEKO-TEX Standard 100.
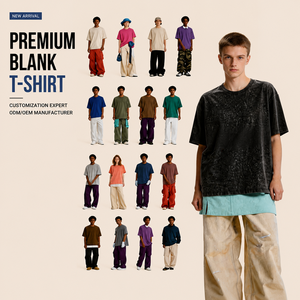
The contemporary San Francisco casual wear market relies heavily on lived-in, vintage-faded textures. Achieving the coveted high-low seam contrast (where seam lines show subtle distressing while body panels maintain deep tone) requires delicate chemical engineering. We combine cationic pigment dyeing with neutral cellulase bio-enzyme stonewashing. This breaks down surface color molecules selectively, creating authentic 90s retro streetwear finishes without structural fabric degradation.
Understanding the chemical mechanics, colorfastness parameters, and economic trade-offs for custom apparel lines.
| Technical Dimension | OEM Custom Garment Dyeing | Traditional Piece/Roll Dyeing | San Francisco Market Advantage |
|---|---|---|---|
| Color Matching Precision | Pantone TPX / TCX Lab Dip matching within ΔE < 0.8 | Standard mill rolls with potential lot-to-lot variance | Enables exact brand color matching for custom drops |
| Seam Abrasion & Contrast | High-low edge fading & distress capabilities (Pigment/Wash) | Flat, uniform color with zero character or seam contrast | Essential for SF vintage streetwear & high-end lounge wear |
| Dimensional Stability | Pre-shrunk during wash cycles; shrinkage guaranteed < 1.5% | Unwashed rolls shrink 3-7% after consumer laundry | Flawless sizing consistency across repeated wash cycles |
| Minimum Order Quantity | Low-MOQ flexibility: 50 pieces per colorway | High mill minimums: 300 - 1,000 kg per color batch | Preserves startup cash flow and prevents over-production |
| Hand-Feel / Softness Index | Ultra-soft, bio-enzyme treated relaxed cotton structure | Stiff sizing agents remaining on finished fabric face | Matches premium SF boutique hand-feel expectations |
How we take your initial moodboard or technical sketch to retail-ready, quality-audited apparel shipments delivered directly to San Francisco fulfillment hubs.
Our CAD pattern master cuts custom sizing blocks tailored to your target demographic—whether relaxed Bay Area streetwear or athletic slim-fit cuts. digital 3D fitting prevents physical sample waste.
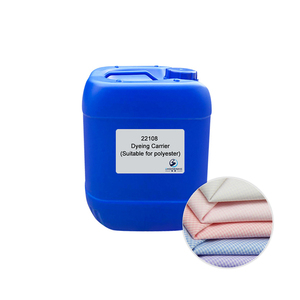
We source or custom-knit PFD (Prepared For Dyeing) organic cottons, heavy french terry, or polyester blends using high-efficiency disperse carrier agents like 22108 for synthetic stability.
Using Pantone TCX/TPX targets or physical swatches, our laboratory formulates custom dye ratios. Lab dips are dispatched to SF via express courier for shade sign-off under D65 lighting.
Garments are stitched using specialized 100% cotton thread or dye-absorbent poly-core thread to ensure seamless seam coloration during the industrial wash process.
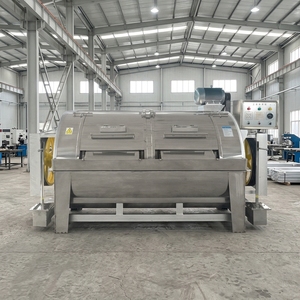
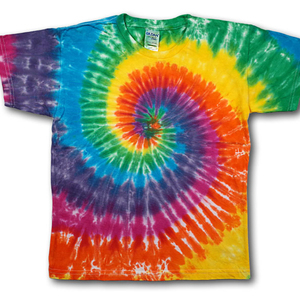
Apparel enters our low-liquor dyeing machinery. Depending on spec, garments undergo reactive dyeing, pigment vintage washing, acid black processing, or custom tie-dye pigment application.
Every unit undergoes dimensional checking, seam pull tests, colorfastness testing (ISO 105), tag attachment, folding, and door-to-door air freight shipping to Northern California.
Real-world OEM manufacturing configurations engineered for Northern California's diverse brand landscapes.
Client Target: Venture-backed tech-lifestyle apparel brand launching a 450GSM heavy hoodie drop.
Dye Strategy: Pigment Grey & Mineral Charcoal Dyeing with neutral enzyme stone wash.
Result: Vintage distressed look with subtle high-low seam accents, pre-shrunk fit, and 50-piece low MOQ batch scaling.
Client Target: Eco-conscious boutique brand emphasizing zero chemical residue.
Dye Strategy: Low-temp Reactive Dyeing with GOTS-certified reactive powders and low liquor ratios.
Result: Deep, vibrant color fastness (Grade 4-5) under heavy sunlight, zero toxic discharge compliance for CA standards.
Client Target: Outdoor activewear label developing fleece jackets and synthetic joggers.
Dye Strategy: High-efficiency Disperse Carrier Agent (22108) combined with acid black powder dyes.
Result: Deep jet-black penetration on hard-to-dye polyester fiber blends with zero bleeding during rain exposure.
Direct technical answers regarding MOQs, turnaround times, environmental standards, and custom development.
Our minimum order quantity starts at 50 pieces per design/colorway for standard cotton knitwear (t-shirts, hoodies, sweatpants). For complex technical fabrics, specialized tie-dye combinations, or disperse-dyed synthetics, mill minimums for specific chemicals may slightly adjust the MOQ. We provide complete transparent cost breakdowns prior to sampling.
Pattern development, lab dips, and initial pre-production sampling generally require 2 to 3 weeks. Once sample approval is granted, bulk manufacturing and garment dyeing takes 3 to 4 weeks. Air express freight directly to San Francisco International Airport (SFO) or Oakland delivery hubs takes 5-7 business days.
Yes. If you do not possess a formal tech pack, our in-house design team can build fully graded measurement specifications, Bills of Materials (BOM), and stitching guidelines from physical reference garments, tech sketches, or digital moodboards.
We utilize digital spectrophotometer color testing to lock in lab dips to strict ΔE thresholds (< 0.8 tolerance). Every industrial dye batch undergoes strict liquor-ratio temperature control and automated dosing of auxiliary agents (such as Direct Black EX or disperse carriers) to guarantee exact match across all sizes.
Absolutely. All dyes, fixatives, and wash chemicals used in our industrial machinery are 100% free of heavy metals, azo dyes, and harmful formaldehyde compounds. We comply fully with OEKO-TEX Standard 100, REACH, and California Proposition 65 standards.
Yes. Our full cut-and-sew ODM service includes post-wash finishing options: custom woven main labels, satin neck tapes, silicone print overlays, high-density embroidery, and customized eco-friendly polybags with barcode stickering ready for Amazon or D2C warehouse distribution.
Partner with an OEM manufacturer that understands San Francisco's quality standards, sustainable requirements, and low-MOQ agility. Request lab dips and custom pricing today.
