Custom-manufactured performance streetwear, tracksuits, hoodies, and vintage athletic wear designed to technical specifications with low 50-piece minimums.
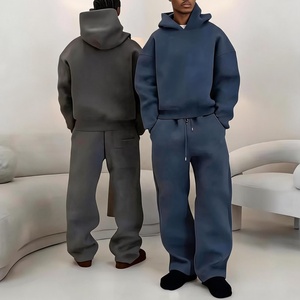
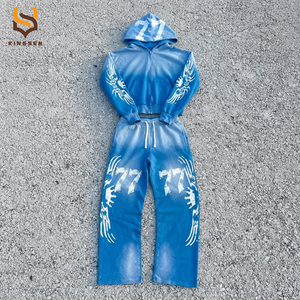
Low Minimum MOQ
Global Brands Scale Up
In-Line Quality Audit
Technical Apparel Expertise
The Greater Boston metropolitan area represents one of North America’s most complex and high-density markets for performance sportswear, athletic wear, and boutique technical apparel. Anchored by world-renowned collegiate athletic programs (NCAA Division I institutions across Cambridge, Chestnut Hill, and Boston proper), an elite marathon endurance community, and a rapidly expanding ecosystem of direct-to-consumer (DTC) athletic apparel startups centered around Kendall Square and the Seaport District, Boston demands an exceptionally high standard of garment engineering, thermal versatility, and supply chain agility.
As a premier custom sportswear supplier and exporter specializing in the North American East Coast corridor, our manufacturing infrastructure bridges the gap between low-volume boutique flexibility and full-scale industrial apparel execution. Unlike commodity blank apparel embellishers, our operation operates as a complete cut-and-sew partner. We deliver full pattern drafting, proprietary fabric knitting, custom yarn dyeing (Pantone-matched), automated precision cutting, and rigorous 4-stage quality control (QC) governed by international ISO 9001 standards and US FTC labeling compliance.
In this technical white paper, we examine the specific material requirements, localized environmental demands, micro-batch manufacturing mechanics, and direct export protocols necessary for apparel brands, athletic directors, and private labels operating within the Greater Boston regional market.
Engineered to meet the exact micro-climate, performance, and aesthetic criteria of New England's athletic ecosystem.
Training along the Charles River Esplanade or competing on the hilly course from Hopkinton to Copley Square demands advanced thermo-regulation. We engineer 3M reflective lightweight nylon windbreakers and ultra-breathable moisture-wicking poly-spandex blends that withstand cold coastal headwinds down to 20°F while preventing moisture buildup during high-aerobic output.
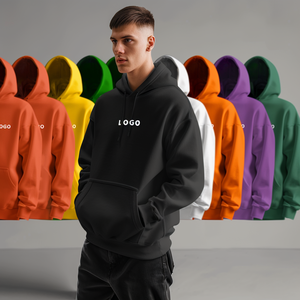
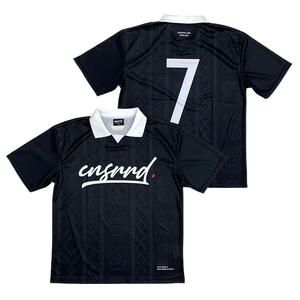
Serving varsity, club, and intramural athletic departments across New England requires high-durability, repeatable pattern specifications. Our factory supplies custom sublimated retro soccer kits, heavy-gauge cotton-blend team hoodies, and travel tracksuits with reinforced flatlock stitching built to endure intensive collegiate training schedules and regional transit.
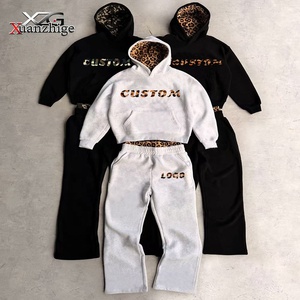
Boston's tech and venture-backed activewear brands rely on hyper-fast iteration cycles and elevated street-to-gym aesthetics. Utilizing custom acid-wash finishes, cropped heavy-fleece hoodies, and custom-dyed organic tech fleeces, we empower emerging DTC labels to drop limited-edition 50-piece capsule collections without high inventory risk.
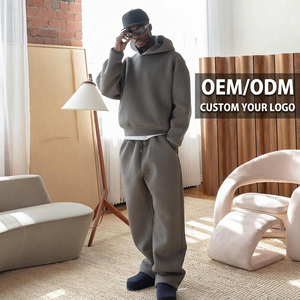
Coastal New England winters introduce high humidity paired with sub-freezing winds. Our double-faced 450 GSM heavyweight cotton-poly fleece tracksuits and windproof water-repellent nylon shells act as thermal barriers for outdoor athletic conditioning, rowing teams on freezing waters, and winter sports enthusiasts.
To succeed in the Boston market, athletic apparel must balance soft handfeel with industrial mechanical performance. Below is an engineering overview of the primary textile configurations manufactured at our facilities:
Critical shifts in consumer purchasing behavior, technical specifications, and procurement strategies across New England.
Traditional 500-1,000 piece factory minimums are obsolete for modern Boston DTC apparel brands. Market leaders are adopting agile micro-batch drops (50–100 pcs per style) to test colors and cuts real-time before scaling bulk re-orders.
Driven by regional sustainability mandates and collegiate procurement guidelines, demand for GRS-certified recycled polyester (rPET) and organic combed cotton has increased by 45% year-over-year in the New England athletic sector.
The line between high-performance gym wear and urban streetwear has dissolved. Heavyweight boxy hoodies, cropped zip-ups, and flared tracksuits with technical inner linings represent the fastest-growing retail category in Boston.
From digital concept validation to customs clearance at the Port of Boston, every step is systematically audited.
Designs, sketches, or tech packs are modeled in 3D to simulate drape, seam tension, and graphic placement prior to cutting fabric.
Patterns are digitally graded across full size spectrums (XS to 3XL) ensuring consistent fit proportions across men's, women's, and unisex cuts.
Textiles are knitted to spec or selected from premium mills, with optional Pantone lab-dip matching to lock in brand colors.
A physical pre-production sample is sewn and shipped for hands-on review, fit-testing, and tactile approval.
Approved samples form the benchmark. Skilled garment workers assemble panels using 4-needle 6-thread flatlock stitching for maximum seam strength.
Garments undergo raw fabric inspection, in-line assembly audits, size-tolerance measurement, and final pre-pack quality checks before air/sea export.
Sourcing offshore apparel manufacturing carries risk when dealing with unverified third-party brokers. We solve this problem by pairing western commercial account management, English-speaking apparel merchandisers, and strict contract law with our own dedicated offshore manufacturing facilities.
Direct technical answers to common procurement questions from Boston athletic buyers and apparel brand founders.
Our baseline MOQ starts at 50 pieces per design. This can be split across standard sizing (e.g., S, M, L, XL). Specialized fabric treatments like custom Pantone yarn-dyeing or intricate acid washes may require higher fabric mill minimums, which our team identifies up front during tech pack evaluation.
We provide full-service DDP (Delivered Duty Paid) or DAP air and ocean freight solutions. Express air delivery to Boston Logan Airport typically takes 5–8 business days following production completion, while sea freight to the Port of Boston takes approximately 25–35 days. All US Customs paperwork, tariff classifications, and duty payments are managed seamlessly.
Yes. Many of our Boston clients send physical reference garments. Our master pattern cutters reverse-engineer the fit, seam construction, and fabric GSM, allowing us to replicate exact fits or upgrade fabric composition according to your brand's requirements.
No. While completed tech packs accelerate the quotation phase, our design team can build spec sheets, graded dimension charts, and bills of materials (BOM) directly from your rough sketches, vector graphics, or sample photos.
Quality control occurs at four critical checkpoints: (1) Raw Fabric Inspection for shade uniformity and structural defects, (2) In-Line Sewing Audits to monitor seam density and stitch strength, (3) End-of-Line Measurement Checks against approved size specs, and (4) Pre-Packaging Audits before cartoning. This guarantees less than a 0.5% defect rate upon arrival in Boston.
All textiles manufactured for the US market comply with Federal Trade Commission (FTC) care labeling rules, CPSIA requirements, and US Customs textile import regulations. OEKO-TEX Standard 100 and GRS certifications are available upon request for eco-conscious product lines.
Get in touch with our B2B apparel merchandisers to review your designs, confirm precise production schedules, and receive an all-inclusive manufacturing quote.
Get a Quote