Explore our complete export portfolio engineered for fashion brands, industrial dye houses, and artisan apparel studios across Luxembourg City, Esch-sur-Alzette, and the Greater Region.
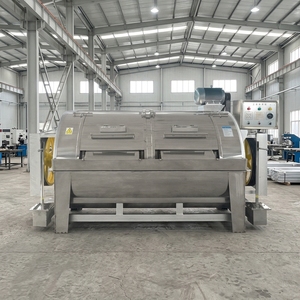
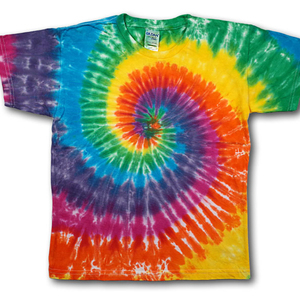
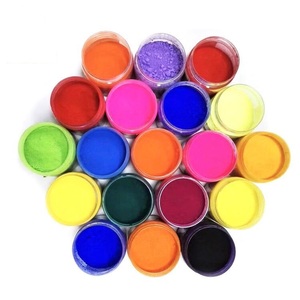
As the apparel sector across the Grand Duchy of Luxembourg shifts toward sustainable luxury, small-batch agility, and eco-certified circular production, traditional roll-dyeing methods present significant inventory risk. Garment dyeing—the technical process of dyeing fully stitched, ready-to-wear apparel from un-dyed RFD (Ready-for-Dye) fabric blocks—offers unprecedented flexibility.
Our operation bridges the precision of UK supply chain governance with the physical execution of our state-of-the-art overseas manufacturing facility. By handling dyeing at the final product stage, Luxembourg fashion houses, corporate merchandise directors, and streetwear labels can hold raw, un-dyed inventory and execute rapid-turnaround colorways based on real-time sell-through data in Luxembourg City, Differdange, or Esch-sur-Alzette.
Traditional fabric dyeing requires ordering thousands of meters of pre-dyed cloth months before consumer trends crystallize. Garment dyeing allows cut-and-sew construction using RFD combed cotton, French terry, or synthetic blends, applying color pigments, reactive dyes, or vintage washes only when order volumes are locked.
Luxembourg consumers prioritize distinct hand-feel and visual texture. Our specialized enzyme washes, acid washes, tie-dye techniques, and pigment garment dyeing deliver soft, lived-in vintage aesthetics without compromising seam strength or structural integrity.
Luxembourg presents one of Europe’s highest GDP per capita retail markets, combined with stringent national environmental directives under the Luxembourg National Energy and Climate Plan (PNEC) and circular economy frameworks. Our export and manufacturing ecosystem addresses specific regional application scenarios:
Boutiques along Avenue de la Liberté and Ville Haute demand heavy-gsm heavyweight tees, hoodies, and sweatpants with custom mineral washes, tie-dye patterns, and precise Pantone-matched reactive shades. We deliver 50-piece low-MOQ runs that allow local labels to drop exclusive capsule collections seamlessly.
Multinational institutions and corporate entities headquartered in Kirchberg require ethically manufactured, GOTS-compliant organic apparel. Our low-water industrial garment dyeing machines and non-toxic direct/acid dye formulations guarantee carbon-reduced corporate merchandise that fulfills ESG reporting criteria.
The academic and technological zone of Esch-Belval demands durable, modern cut-and-sew workwear. Utilizing carrier-assisted disperse dyeing for synthetic workwear and reactive black dyes for knitwear, we engineer colorfastness rated 4-5 against repeated industrial laundering.
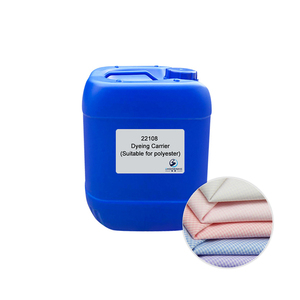
For local textile finishing houses within Luxembourg and bordering regions (Trier, Metz, Arlon), we export specialized textile dye chemicals, including direct black powders, high-efficiency polyester carrier agents, and optical chameleon pigments.
Exporting garments and chemical agents into Luxembourg requires absolute adherence to European Union directives and local environmental laws. As an established international exporter, our technical workflow guarantees zero friction at EU customs checkpoints.
All dye formulations, pigments, and finishing chemicals are strictly free from Azo dyes, heavy metals, formaldehyde, and banned aromatic amines listed under Annex XVII of REACH (EC No 1907/2006).
Our industrial garment dyeing machinery operates at ultra-low liquor ratios (1:5 to 1:8), drastically reducing water and thermal energy consumption per kilogram of finished apparel.
Leveraging Luxembourg’s Eurohub Sud multimodal rail-road terminal in Bettembourg, bulk export shipments are routed directly from port facilities into Luxembourg within optimal transit windows.
Before cutting fabric or running dye batches, clients receive 3D digital renderings and lab-dip color swatches, avoiding wasteful pre-production physical revisions.
From technical drawing (Tech Pack) to packed delivery cartons, every order follows a rigorous engineering methodology to maintain absolute shade consistency across batch iterations.
Analysis of your design spec, sizing reference, and Pantone TCX/TPG color codes. Spectrophotometer lab-dips are produced for physical shade approval.
Pattern cutting and hand-stitching of Ready-for-Dye garments using 100% cotton thread to ensure uniform dye absorption across all seams.
Garments are loaded into automated industrial dyeing machines. Temperature, pH, and auxiliary dosing are monitored via digital PLC controllers.
Bio-enzyme washing for texture enhancement, followed by eco-friendly color fixing agents to secure rubbing and wash fastness standards.
Industrial rotary drying sets the final garment dimensions, effectively eliminating future post-consumer shrinkage.
Inspection of fabric integrity, seam strength, dimensional tolerance measurement against size charts, and final steam ironing/packaging.
Sourcing garment manufacturing overseas often introduces risks regarding legal recourse, communication barriers, and quality variations. Our unique structure solves these structural industry vulnerabilities:
Our sales management, merchandising teams, and design consultancies operate under strict UK corporate contract governance. Simultaneously, bulk manufacturing occurs in our owned overseas facility, delivering direct-from-factory pricing without intermediary markup fees.
While standard Asian and European industrial dye houses mandate minimum order runs of 500 to 1,000 units per color, we support scaling brands by accepting custom orders starting at just 50 pieces per design, spread across multiple sizes.
If your brand lacks technical production files, our pattern masters generate full technical tech packs, size grading charts, and bill-of-materials from physical sample garments, sketches, or mood boards.
Combine specialized garment dyeing with custom woven neck labels, screen printing, high-density embroidery, custom drawcords, branded metal hardware, and retail-ready eco-polybags.
Direct technical answers to the most common questions raised by supply chain managers, brand directors, and buyers in Luxembourg.
Our baseline MOQ starts at 50 pieces per design for standard cotton apparel (such as t-shirts, hoodies, and sweatshirts). Custom-knitted fabrics, complex multi-fiber compositions, or specialized chemical treatments may adjust this threshold based on dye vat minimum capacities.
All goods exported to Luxembourg are supplied with complete commercial invoices, HS commodity code classifications, Certificate of Origin documents, and EU compliant packing lists. Orders can be shipped under DDP (Delivered Duty Paid) terms or DAP via major courier networks (DHL, FedEx, UPS) directly to your Luxembourg business address.
Yes. We utilize computerized spectrophotometers to match your specified Pantone TCX, TPG, or PMS reference numbers. We provide physical lab-dip fabric swatches (or 3D digital swatches) for client sign-off prior to bulk vat dyeing.
Absolutely. Every dye powder, liquid pigment, disperse carrier, and washing auxiliary exported or used in our garment production is 100% REACH compliant and free from hazardous substances, heavy metals, or banned Azo compounds.
Pattern development, tech pack creation, and lab-dip sampling typically require 2 to 3 weeks. Once samples are approved, bulk garment dyeing and construction require 4 to 6 weeks, depending on order complexity and total units.
Garment dyeing inherently preshrinks apparel because garments undergo hot water dyeing, washing, and industrial tumble drying during processing. Residual dimensional shrinkage is controlled to within strict industry standards (< 3%).
Connect directly with our UK-managed merchandising and technical production team. Receive quick quotes, request lab-dip swatches, or download our complete product and chemical catalog today.
Get Catalog