India's industrial economy is undergoing an unprecedented surge, driven by massive infrastructure investments, the national "Make in India" initiative, expanded oil & gas refineries in Gujarat, electronics manufacturing in Tamil Nadu, and heavy mining corridors across Odisha and Jharkhand. Concurrently, environmental health and safety (EHS) mandates enforced by bodies like the Directorate General of Mines Safety (DGMS) and the Bureau of Indian Standards (BIS) are compelling enterprises to shift from generic uniform blanks to specialized, certified custom workwear.
Procuring workwear for the Indian subcontinent presents unique engineering challenges: textiles must withstand extreme ambient heat (exceeding 45°C in summer), high relative humidity during monsoon cycles, abrasive mechanical friction, and rigorous industrial wash cycles. As an international custom apparel manufacturer combining UK-standard quality assurance with agile offshore production lines, we supply Indian industrial enterprises, start-ups, and OEM distributors with precision-crafted, low-MOQ workwear designed for longevity, thermal ergonomics, and total regulatory compliance.
Explore our flagship custom workwear categories engineered for heavy construction, petrochemical refineries, logistics operations, and corporate office environments in India.
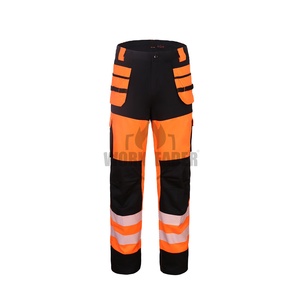
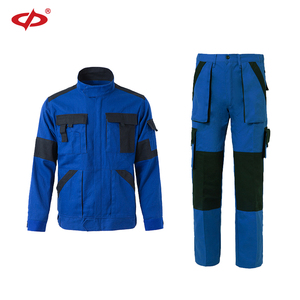
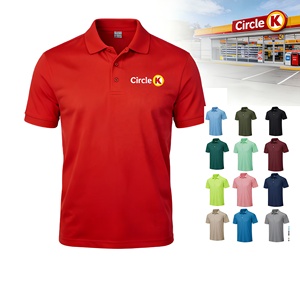
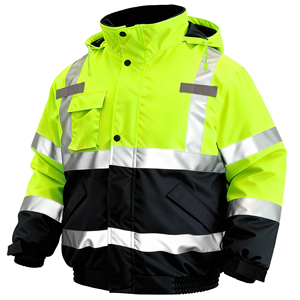
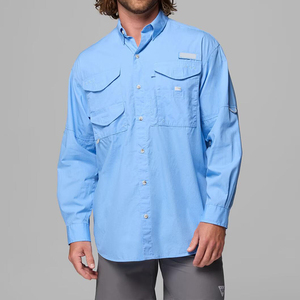
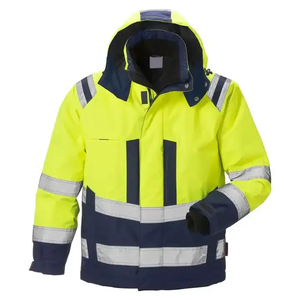

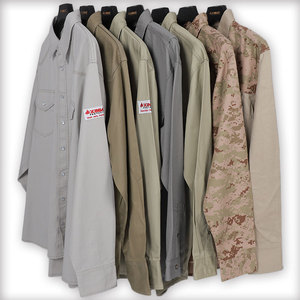
Manufacturing for the Indian enterprise market demands deep localized knowledge of regional operational realities. A single workwear specification cannot address the wet humidity of coastal refineries in Gujarat and the freezing temperatures of Himalayan infrastructure corridors. Below is how our technical garment designs align with India’s primary industrial hubs:
Industry focus: Oil refineries, chemical plants, and heavy fabrication (Jamnagar, Dahej, Hazira, Navi Mumbai).
Requirement: Certified Flame-Retardant (NFPA 2112, IS 15748) coveralls and anti-static ESD shirts engineered with light 200–240 GSM breathable cotton to reduce heat stroke risks in 42°C+ summer environments.
Industry focus: Civil construction, highway corridors, and urban transit systems (Delhi NCR, Bengaluru, Hyderabad).
Requirement: High-visibility Class 2 and Class 3 safety vests and heavy cargo trousers with 3M reflective tape, tear-resistant ripstop fabrics, and ergonomic gusseting for intense physical movement.
Industry focus: Auto plants, electronics assembly, and modern warehousing (Sriperumbudur, Oragadam, Hosur, Pune).
Requirement: Moisture-wicking polo shirts, soft-shell mechanic jackets, and stretch work cargo pants featuring anti-scratch nylon buttons to prevent vehicle body panel damage during assembly.
Industrial procurement managers in India are abandoning legacy, low-cost uniform suppliers in favor of technical manufacturing partners who bring compliance documentation, durability testing, and sustainable sourcing. Four major shifts define current Indian market demand:
Traditional thick canvas uniforms cause severe heat exhaustion among workers. Modern enterprises are switching to high-air-permeability weaves, underarm mesh venting, and bamboo-cotton or poly-spandex blends with UPF 50+ protection.
Leading Indian MNCs and export-driven units require GOTS-certified organic cotton, recycled polyester (rPET) from ocean-bound plastics, and AZO-free non-toxic dyes to comply with global ESG auditing standards.
Compliance with Bureau of Indian Standards (BIS) norms—such as IS 15748 for thermal protection and IS 15809 for high-visibility warning clothing—is now mandatory in corporate risk management frameworks across India.
Compare our specialized fabric formulations optimized for high-temperature durability, chemical protection, and corporate identity across Indian operating conditions:
| Fabric Blend | GSM Range | Key Performance Attribute | Compliance Rating | Recommended Application |
|---|---|---|---|---|
| 100% Treated FR Cotton | 220 - 350 GSM | Inherent flame resistance, high thermal comfort | NFPA 2112, IS 15748, EN 11612 | Welding, Petrochemical, Steel Foundries |
| 65/35 Poly-Cotton Ripstop | 240 - 280 GSM | High tear strength, colorfastness against strong sunlight | ISO 13934-1, AATCC 61 | Heavy Construction, Mining, Civil Defense |
| Piqué Poly-Spandex Blend | 180 - 220 GSM | 4-Way stretch, rapid moisture evaporation | UPF 50+, OEKO-TEX Standard 100 | Corporate Delivery, Logistics, Field Techs |
| 300D Oxford Waterproof TPU | 300 GSM | Hydrostatic pressure resistance >10,000mm | EN 343 Class 3:1, IS 15809 | Monsoon Infrastructure, Outdoor Security |
Bridging the gap between premier UK account management standards and high-efficiency offshore manufacturing, we eliminate the agency middleman to deliver custom industrial garments directly to your facility.
Unlike traditional factories mandating 1,000+ units, our minimum order starts from just 50 pieces per design. This enables enterprise buyers to run localized site pilots and small-batch drops without locking up working capital.
Every unit undergoes strict auditing: raw fabric inspection for shade & GSM, in-line seam tension testing, end-of-line dimensional measurement against graded tech packs, and pre-pack audit prior to shipping.
Don't have a tech pack? Our in-house design team converts your rough sketches, physical reference samples, or brand guidelines into production-ready 3D digital renderings and graded sizing charts.
From exact Pantone color-matching to customized woven labels, heavy embroidery, screen printing, and high-tensile reflective striping, we retain complete creative and functional control over your garments.
Clear, direct answers regarding custom manufacturing, logistics, compliance, and ordering procedures for India-based businesses.
We work with global logistics partners (DHL, FedEx, and specialized air/sea freight forwarders) to handle door-to-door delivery across major Indian cities including Mumbai, Nhava Sheva, Delhi NCR, Chennai, and Bengaluru. We provide complete commercial invoices, packing lists, and HS Code classifications (e.g., Chapter 62 for apparel) to ensure seamless customs clearance through Indian ICEGATE systems.
Yes. Our FR apparel utilizes fabrics tested to meet both international standards (NFPA 2112, EN ISO 11612) and Indian equivalents (IS 15748). Our high-visibility workwear complies with IS 15809 / EN ISO 20471. Test certificates and lab reports are provided alongside pre-production samples upon request.
Absolutely. Our low Minimum Order Quantity (MOQ) starts from 50 pieces per design. This allows Indian safety officers and enterprise buyers to deploy trial uniforms in real working conditions, verify durability and worker feedback, and make sizing adjustments before placing high-volume repeat orders.
Standard European or American size charts often result in poor fit for Asian and Indian body proportions (e.g., oversized sleeve lengths or tight waist ratios). We maintain specific "Asian / Indian Ergonomic Fit" grading templates, ensuring comfort, freedom of movement, and professional aesthetic appeal on site.
Pattern creation and physical sample delivery generally take 2 to 3 weeks. Upon final sample approval, bulk manufacturing requires 4 to 6 weeks depending on custom dyeing or compliance treatments. Express air freight delivers orders to India in 4 to 7 business days, while sea freight takes approximately 18 to 25 days.
We engineer textiles specifically for tropical and extreme industrial environments. We use long-staple combed cotton, bio-washed finishes, and synthetic blends featuring high Moisture Vapor Transmission Rates (MVTR). Underarm mesh inserts, ventilated back yokes, and anti-bacterial treatments keep workers cool, dry, and odor-free throughout 12-hour shifts.
Partner with a global manufacturing leader that understands India's industrial requirements. Low minimums, certified fabrics, and UK-standard quality control delivered to your site.
Get Catalog